Home

Blog

Blog

  • Small Cracks Appear on the Surface of Alloy Blades After Use — Can They Still Be Used?
    Jul 03, 2026
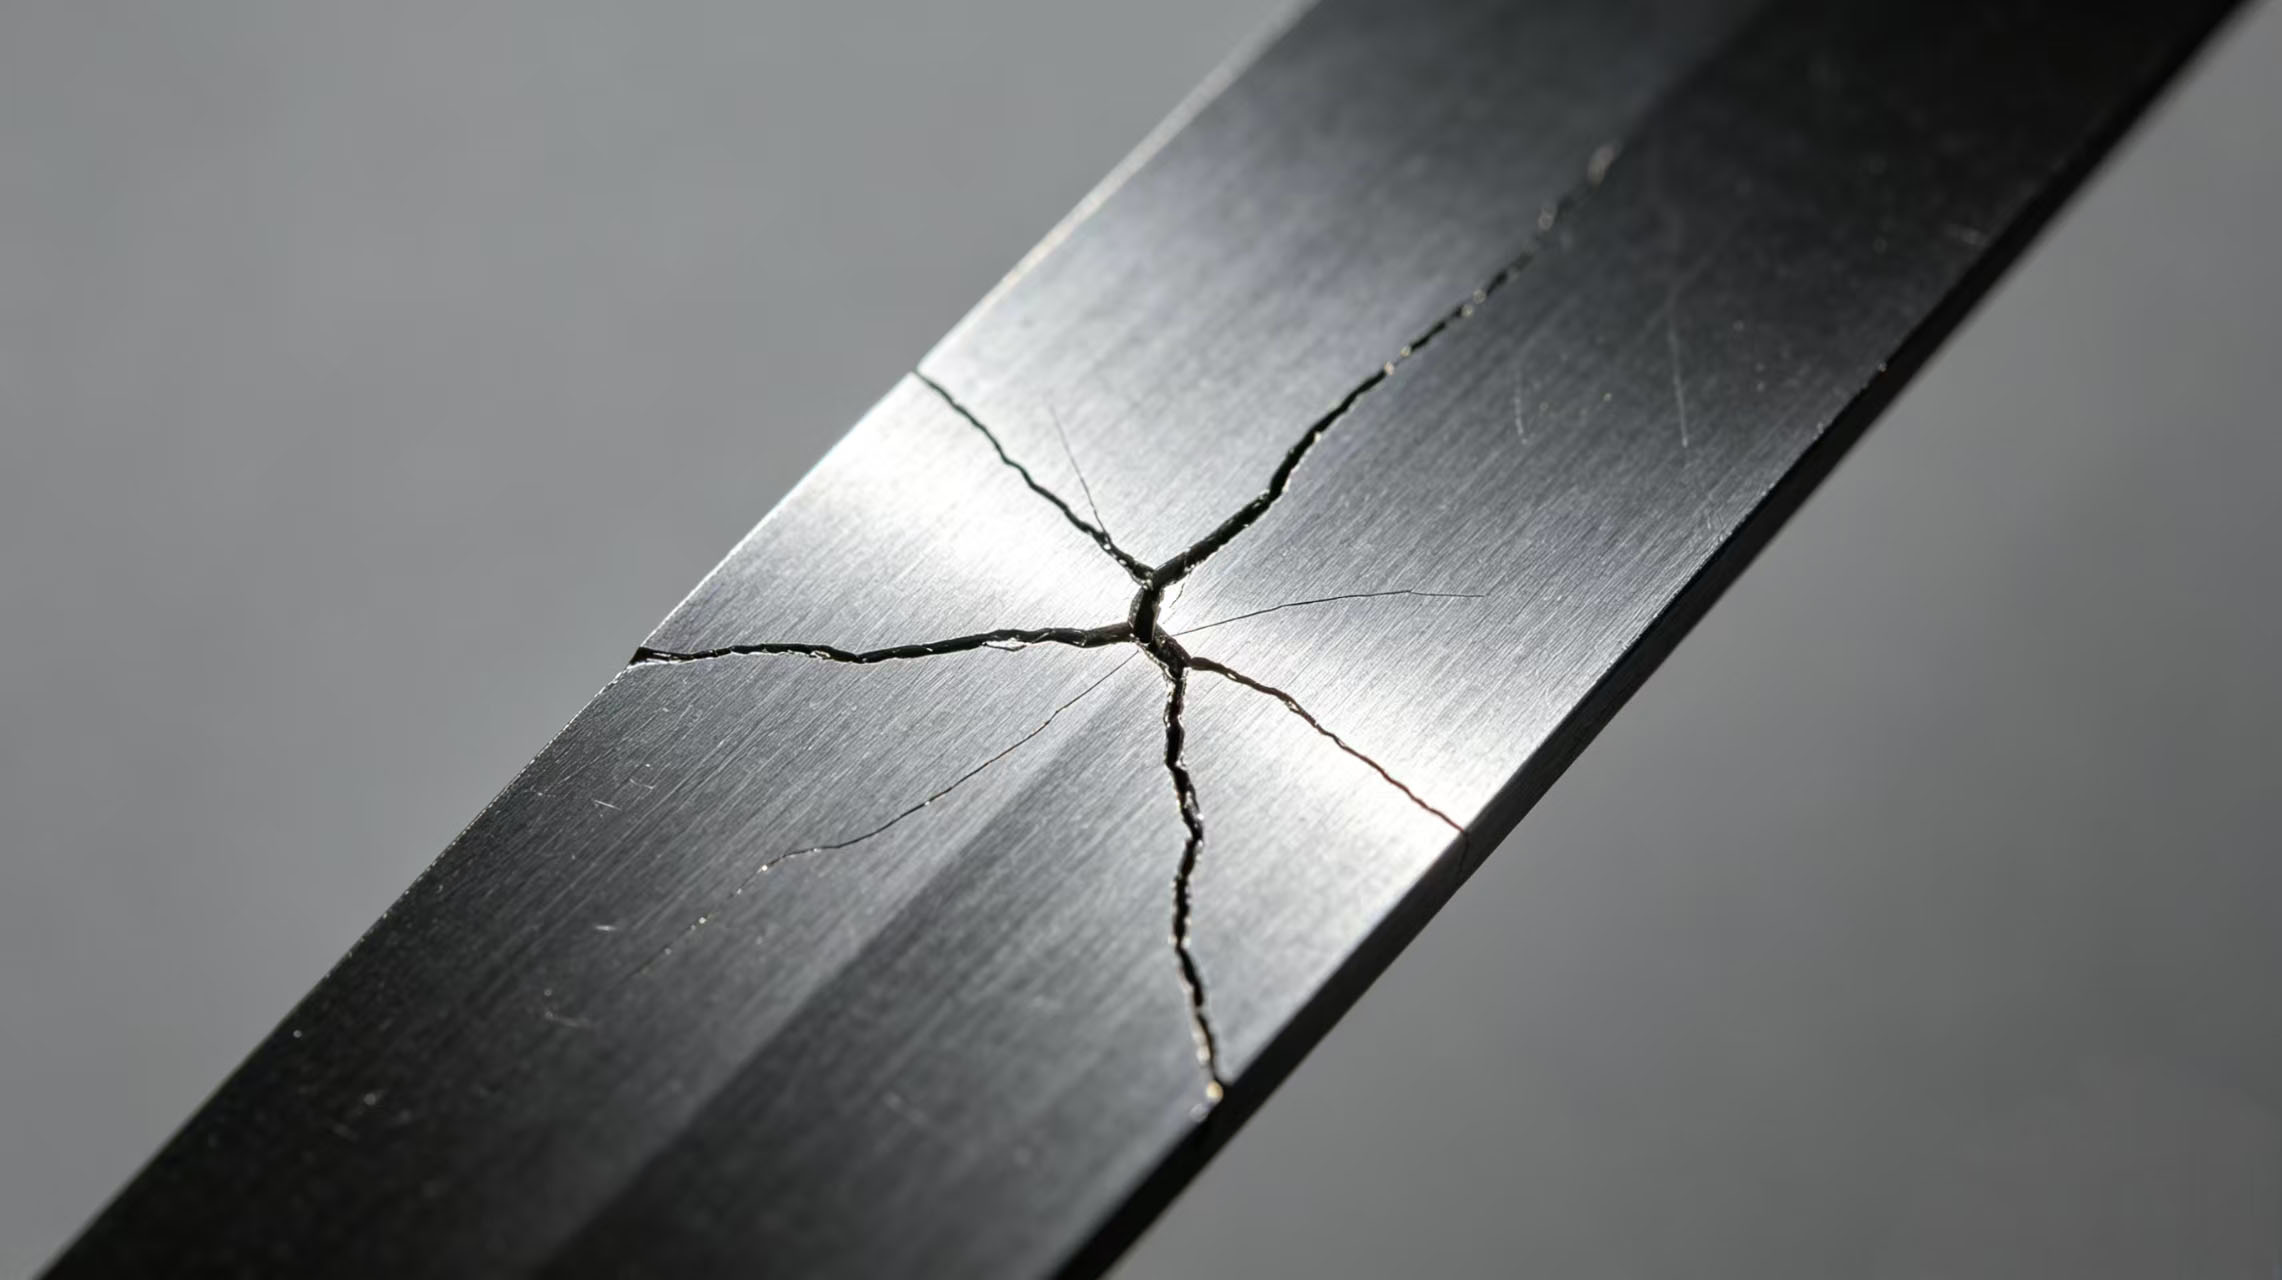
    In slitting production, operators occasionally find small cracks on the surface of alloy blades. Some of these cracks are visible to the naked eye, while others can only be seen with a magnifying glass. When encountering such a situation, many people's first reaction is, "Can it still be used?" Mingbai Mechanical Tool Technology Co., Ltd., based on materials science and field experience, provides you with judgment criteria and handling recommendations.   1. Two Types of Cracks: Surface Cracks vs. Deep Cracks   Surface micro-cracks: The depth is usually less than 0.05mm, existing only in the blade's surface layer. Such cracks may be caused by grinding thermal stress, coating shrinkage stress, or minor impact. If the crack does not extend to the edge and the blade material is a tough high-speed steel blade, it may be temporarily usable under low-load conditions.   Deep cracks: Depth exceeds 0.1mm, or extends from the surface inward. Such cracks often originate from excessive heat treatment stress, quenching micro-cracks, or long-term fatigue. Once a deep crack appears, a carbide blade may fracture completely at any time and must be taken out of service immediately.   2. Common Causes of Cracks   1. Grinding burn During resharpening, excessive feed rate or insufficient cooling causes localized overheating, producing grinding cracks. Such cracks are usually network-like or fine linear, distributed near the edge. Common in precision slitting circular blades.     2. Heat treatment defects Quenching temperature too high or inadequate tempering leaves excessive residual stress inside the blade, which slowly releases during use and causes cracking.   3. Fatigue cracks Alloy blades for silicon steel slitting are subjected to alternating cutting stress over long periods, and fatigue cracks initiate at stress concentration points.   4. Impact cracks The blade receives an unexpected impact (such as material joints or hard inclusions), causing localized chipping that extends into a crack.   5. Coating cracks PVD coatings are hard but brittle. Under significant impact, the coating may crack while the substrate remains intact. Such cracks only affect coating life; the substrate of coated alloy blades can continue to be used.   3. Three-Step Method to Determine Whether It Can Still Be Used   Step 1: Identify the crack location   · Crack on the edge → Dangerous, pieces may fly off during cutting, must be taken out of service. · Crack in a non-stressed area of the blade body, such as near the bore → Lower risk, can be used with short-term monitoring. · Crack on the end face but not extending to the outer diameter → Further depth inspection needed.     Step 2: Assess crack depth   · Observe with a 10x or higher magnifying glass. If the crack is as fine as a hair and does not penetrate the surface → it may be a surface crack. · Use dye penetrant inspection: clean the blade, apply penetrant, wipe off, then apply developer. If the developing line is continuous and clear → the crack is relatively deep. · Gently scrape with a fingernail or a metal piece. If you can feel a noticeable groove → the depth may exceed 0.1mm.     Step 3: Decide based on working conditions   · Low speed, low load, non-safety-critical position → a surface crack may be temporarily usable, but increase inspection frequency. · High speed, high load, automated production line → any crack is recommended to be taken out of service. · Cutting valuable materials or involving personnel safety → replace immediately.   4. Crack Tolerance for Different Blade Materials   · High-speed steel blades: Good toughness, surface micro-cracks can be used short-term with monitoring. · Carbide blades: Very brittle, any crack is recommended to be taken out of service. Cracks in carbide propagate extremely quickly.     · Stainless steel blades: Best toughness, relatively higher tolerance for surface cracks. · Coated blades: If only the coating is cracked and the substrate is intact, they can continue to be used, but the protective effect of the coating is reduced.   5. Emergency Handling for Cracked Blades   If you must temporarily use a custom slitter blade with a crack, follow these rules:   1. Reduce cutting speed to below 60% of normal. 2. Decrease blade gap and overlap to reduce impact. 3. Stop every 30 minutes to check whether the crack has propagated. 4. Install a protective guard around the blade.   6. How to Prevent Cracks?   · Standardize resharpening: Send back to factory for CNC grinding, control feed rate and cooling to avoid grinding burn. · Optimize heat treatment: Choose suppliers with metallographic inspection capability to ensure adequate tempering. · Select appropriate material: For high-impact conditions, choose tougher wear-resistant circular blades. · Inspect before installation: Check each new blade's edge and surface with a magnifying glass.   7. Mingbai Technology's Recommendations and Inspection Services   Mingbai Mechanical Tool Technology Co., Ltd. recommends that any crack extending to the edge, or any crack deeper than 0.1mm, should be taken out of service immediately. For cracks where the depth cannot be determined, you can send the blade back to Mingbai's laboratory for dye penetrant inspection or magnetic particle inspection. We will issue an inspection report clearly marking the crack's location, length, and depth, and give a conclusion of usable or scrap.     Conclusion   Small cracks do not mean immediate scrap, but they should never be taken lightly. Location, depth, working conditions, and material together determine the fate of a cracked blade. When you are unsure, the safest choice is to take it out of service, inspect it, and consult a professional manufacturer. Mingbai Technology is willing to provide crack inspection and risk assessment services for you. Website: www.mingbaiblade.com
  • When Slitter Blades Produce Sharp Noise During Cutting, Is It a Blade Problem or an Equipment Problem?
    Jun 30, 2026
    In metal slitting operations, a sudden sharp, piercing noise from slitter blades during cutting is an alarming signal. Such noise not only affects the working environment but also often indicates potential issues with the blade or equipment. Many operators struggle to identify the source of the noise, blindly replacing blades or stopping production for inspection, which wastes time and increases costs. Mingbai Mechanical Tool Technology Co., Ltd., based on extensive on-site diagnostic cases, helps you quickly determine: does the sharp noise come from the blade or the equipment?   1. Two Typical Sources of Sharp Noise     1. High-frequency continuous screeching sound (similar to metal scraping)   This sound is continuous, sharp, and usually related to the rotational frequency of the blade or blade shaft. Common causes:   · Blade gap too small, upper and lower edges rubbing against each other · Insufficient lubrication, dry friction between blade and material · Edge clearance angle too small, excessive contact area between blade body and material · Blade surface roughness too high, resulting in high friction coefficient   2. Periodic impact sound (similar to a "click" or "clack")   This sound occurs rhythmically, once or several times per revolution. Common causes:   · Blade edge has chipping; the chipped area impacts the material during rotation · Blade or blade shaft eccentricity, producing an impact each revolution · Excessive clearance between blade bore and blade shaft, causing the blade to wobble on the shaft   2. Three-Step Diagnosis: Blade or Equipment?   Step 1: No-load test     Remove the material and let the slitter blades run at no load. If the noise disappears → the problem lies with the material or cutting parameters. If the noise persists → the problem lies with the blade or equipment.   Step 2: Exchange test   Move the noisy circular blade to another normal machine and run it. If the noise follows the blade → the problem is with the blade itself. If the noise stays with the original machine → the problem is with the equipment.   Step 3: Component-by-component inspection   · Remove the blade and rotate the blade shaft alone; listen for abnormal bearing noise. · Check blade shaft runout (measure with a dial indicator; radial runout should be ≤0.005mm). · Check blade gap (measure with a feeler gauge; should be 5%-10% of material thickness).   3. Blade-Related Noise Issues   1. Edge chipping   Circular blades for stainless steel strip slitting may develop tiny edge chips when encountering hard spots in the material. When the chipped area rotates into contact, it impacts the material, producing a periodic "clack" sound.     2. Uneven edge wear   Alloy blades for silicon steel slitting are prone to localized wear bands due to the hardness of the material. The alternating contact of worn and unworn areas with the material produces a periodic screeching sound.   3. Coating peeling   After the PVD coating of high-speed slitter blades peels off, the exposed substrate has a higher friction coefficient with the material, generating a continuous screeching sound.   4. Blade deformation   Ultra-thin circular blades may develop end face warpage during heat treatment or use, causing the edge trajectory to become wavy during rotation and producing high-frequency noise.   4. Equipment-Related Noise Issues   1. Bearing damage   When spindle bearings are worn or pitted, the rolling elements passing over damaged areas produce high-frequency vibration and screeching, intensifying with increasing speed.     2. Bent blade shaft   A slightly bent blade shaft creates a radial impact once per revolution, producing a rhythmic impact sound.   3. Excessive gear backlash   Worn transmission gears with increased backlash produce impact noise during gear meshing under cutting loads.   4. Lubrication system failure   Insufficient lubricant or blocked oil passages cause bearings and gears to run under dry conditions, producing metal-on-metal screeching sounds.   5. Solutions   Blade issues:   · Chipping or wear → return to factory for resharpening or replacement. · Coating peeling → recoat or replace with custom slitter blades. · Deformation → check flatness; scrap if out of tolerance.   Equipment issues:   · Bearing damage → replace spindle bearings and inspect the blade shaft. · Bent blade shaft → straighten or replace. · Lubrication system → clean oil passages and replace lubricant.   6. Mingbai Technology's Diagnostic Services   Mingbai Mechanical Tool Technology Co., Ltd. offers noise diagnostic services:   · Free remote audio diagnosis (record the equipment running sound and send it to us). · On-site vibration testing using a vibration meter to capture spectrum data. · Issue a diagnostic report clearly identifying the noise source and providing solutions. · Provide noise reduction recommendations (gap adjustment, lubrication improvement, blade selection).     7. Case Study   A stainless steel strip slitting plant experienced a sharp, continuous piercing noise from circular blades for precision slitting during cutting. The customer tried blades from three different suppliers, but the noise persisted. Mingbai engineers inspected on-site and found that the radial clearance of the lower blade shaft bearing was 0.08mm (standard ≤0.02mm), and the bearing cage had fractured. After bearing replacement, the noise completely disappeared.   Conclusion   When slitter blades produce sharp noise during cutting, it could be a blade problem or an equipment problem. Use the three-step method of "no-load test + exchange test + component-by-component inspection" to quickly locate the source. Mingbai Technology is ready to help you eliminate noise and restore smooth production with our professional diagnostic capabilities. Website: www.mingbaiblade.com
  • What Hidden Conditions Lie Behind Mechanical Blade Manufacturers' Promises of "Free Resharpening"?
    Jun 29, 2026
    When purchasing custom blades, circular blades, or slitter blades, many manufacturers advertise "free resharpening" to attract customers. It sounds like a great deal — send the dull blade back for resharpening at no cost. However, Mingbai Mechanical Tool Technology Co., Ltd. reminds you: free resharpening does not mean unconditional resharpening. This article reveals the common restrictions hidden behind "free" offers.   1. Why Do Manufacturers Offer "Free Resharpening"?   · To attract long-term cooperation and increase customer loyalty · To understand customer usage patterns through resharpening and gain reorder opportunities · To identify blades reaching the end of their life during resharpening and generate new orders   2. Six Most Common Hidden Conditions     1. Only the first resharpening is free   Many manufacturers' "free resharpening" actually only covers the first resharpening, with subsequent sharpenings incurring charges. A circular blade for precision slitting typically requires 3-5 resharpenings over its entire lifecycle.   2. Only normal wear, not abnormal damage   If a blade has chipping, cracks, deformation, or other abnormal wear, the free resharpening service is usually not applicable. Manufacturers will classify these as "improper use" and require paid repair or direct scrapping.   3. Resharpening frequency tied to remaining blade thickness   When the cumulative resharpening removal exceeds 10%-15% of the original thickness, manufacturers may refuse further resharpening, claiming the blade has "reached its life limit." However, for high-speed steel custom blades, a reasonable number of resharpenings should be higher.   4. Shipping costs are not included   "Free resharpening" often does not include shipping costs. A heavy-duty slitter blade can weigh dozens of kilograms, and round-trip shipping may exceed the value of the resharpening itself.     5. Minimum return frequency requirements   Some manufacturers require customers to return blades for resharpening a certain number of times per year, or they will revoke the free eligibility. This is difficult for users of alloy blades for small-batch slitting to meet.   6. No performance guarantee after resharpening   The most hidden condition is that some manufacturers do not provide inspection reports after free resharpening and do not guarantee precision indicators such as angle and runout. The resharpened precision mechanical blade may perform worse than before.     3. How to Avoid These Pitfalls?   · Clarify before signing: the number of free resharpenings, scope, and shipping cost responsibility. · Request a resharpening report: provide angle and runout comparison data before and after each resharpening.     · Define abnormal damage clearly: what counts as "abnormal" chipping and what counts as "normal" wear. · Keep original inspection records: to serve as a basis for comparison after resharpening.   4. Mingbai Technology's Resharpening Policy   Mingbai Mechanical Tool Technology Co., Ltd. provides transparent resharpening services:   · First resharpening is free (including shipping) · Subsequent resharpenings are clearly priced by blade diameter and material, with no hidden fees · Each resharpening comes with an inspection report showing before-and-after data · Abnormal damage is communicated in advance, and the customer decides whether to repair or scrap · No minimum return frequency threshold — resharpening is performed as needed     5. Cost Comparison   Taking a custom slitter blade worth 800 RMB as an example, with 4 resharpenings over its lifecycle:   · "Free" resharpening plan: first time "free," subsequent 3 times at 300 RMB each plus shipping, no resharpening reports, total approximately 900 RMB plus shipping. · Mingbai transparent resharpening plan: first time free including shipping, subsequent 3 times at 200 RMB each with clear pricing, each with a resharpening report, total 600 RMB.     Conclusion   "Free resharpening" sounds appealing, but hidden conditions often exist behind it. When choosing blades, you should not only look at the purchase price, but also consider the full lifecycle resharpening costs and service transparency. Mingbai Technology provides a transparent resharpening policy, ensuring you understand every expense clearly. For detailed resharpening pricing, please request our price list. Website: www.mingbaiblade.com
  • When Shearing Different Thickness Materials with Circular Blades, Is Separate Customization of the Edge Necessary?
    Jun 23, 2026
    In slitting production, many users encounter this puzzle: the same equipment and the same set of circular blades work perfectly on 0.5mm material, but when switching to 1.5mm of the same material, problems such as burrs, tearing, and even chipping occur. They then ask: when shearing different thickness materials with circular blades, is separate customization of the edge necessary? Mingbai Mechanical Tool Technology Co., Ltd. answers: Not necessarily every time, but when the thickness difference exceeds a certain range, customization is necessary. This article provides a detailed analysis.   1. The Impact of Thickness Differences on Edge Requirements   1. Relationship between edge angle and cutting resistance   The edge angle (wedge angle) determines the sharpness and strength of the blade:   · Thin materials (<0.5mm) require a small angle (18°-22°) to maintain sharpness; otherwise, they won't cut through. · Thick materials (>2mm) require a large angle (25°-30°) to ensure edge strength; otherwise, chipping occurs.   If circular blades for thin sheet slitting are used to cut thick plates, the edge is too sharp and prone to chipping. If high-speed steel blades for thick plate shearing are used to cut thin sheets, the edge is too dull, resulting in large burrs on the cut edge.     2. Edge radius and material deformation   The edge radius (passivation value) determines the degree of extrusion when penetrating the material:   · Thin materials require an extremely small edge radius (R≤0.005mm) to minimize material deformation. · Thick materials require a slightly larger edge radius (R=0.01-0.02mm) to enhance edge impact resistance.   3. Chain reaction of gap and overlap changes   When thickness changes, the blade gap and overlap must be reset. However, if the edge design is unreasonable, even adjusting parameters will make it difficult to achieve the ideal cutting effect.     2. When Is Separate Edge Customization Necessary?   1. Thickness difference exceeds 3 times   For example, if the same equipment is used to cut both 0.3mm and 1.0mm materials, the edge angle and radius requirements are completely different. Two sets of stainless steel strip slitting circular blades should be customized.   2. Completely different material properties   Even with the same thickness, different materials (e.g., copper strip vs. stainless steel strip) have different edge requirements. Circular blades for copper strip cutting require extremely sharp, anti-adhesion edges, while alloy blades for silicon steel slitting require wear-resistant edges.   3. Different equipment rigidity   Old equipment with poor rigidity requires a duller edge to absorb impact; new equipment with sufficient rigidity can use a sharper edge. If two sets of equipment share the same high-precision custom blades, the results will inevitably differ.   3. When Is Customization Not Necessary?   · Thickness difference within ±50% (e.g., 0.8mm and 1.2mm): use a medium edge angle and adjust the gap. · Both are within the thin material range (0.3-0.8mm) or within the thick material range (1.5-3mm): only fine-tuning the gap is needed; no separate edge customization is required.     4. Mingbai Technology's "One Material, One Edge" Customization Solution   Mingbai Mechanical Tool Technology Co., Ltd. provides targeted customization services:   1. Customer provides material grade, thickness range, and equipment model. 2. Mingbai engineers calculate the optimal combination of edge angle, radius, and clearance angle. 3. Produce the corresponding custom slitter blades and attach an edge inspection report.     If the same equipment needs to cut multiple thicknesses, we can provide a "multi-edge blade set for different thicknesses" with laser marking on the blade indicating the recommended thickness to avoid misuse.   5. Case Comparison   A copper strip slitting plant used the same set of wear-resistant circular blades to cut 0.2mm and 0.8mm copper strips. Cutting 0.2mm produced smooth edges, but cutting 0.8mm resulted in severe burrs and halved blade life. Mingbai Technology customized two sets of slitting circular blades with different edges: 18° sharp edge for thin material, 25° wear-resistant edge for thick material. By switching blades when changing materials, burrs disappeared, and total blade life increased by 40%.     Conclusion   When shearing different thickness materials with circular blades, separate edge customization is not always necessary. However, when the thickness difference exceeds 3 times, material properties differ, or equipment rigidity varies significantly, customizing the edge is essential to ensure cutting quality. Mingbai Technology is committed to providing professional "one material, one edge" matching solutions, ensuring you get excellent results whether cutting thin or thick materials.   Website: www.mingbaiblade.com
  • Can Poor Dynamic Balance of Slitter Blades Damage the Equipment Spindle?
    Jun 22, 2026
    The answer is: Yes, and the consequences are more serious than you might imagine. Many slitting plants focus only on blade material and edge sharpness, but overlook the critical indicator of dynamic balance. Slitter blades with poor dynamic balance generate centrifugal forces during high-speed operation that act like "high-frequency hammering" continuously impacting the spindle bearings. Over time, this leads to loss of spindle precision, bearing damage, and even complete machine failure. Mingbai Mechanical Tool Technology Co., Ltd. provides a detailed analysis of the hazards of poor dynamic balance and their solutions.   1. How Does Poor Dynamic Balance Damage the Spindle?     When a high-speed slitter blade has a mass eccentricity, it generates a centrifugal impact with each revolution. At 300 RPM, this equates to approximately 430,000 impacts per day; at 1000 RPM, the number of daily impacts reaches as high as 1.44 million.   These impacts are transmitted through the blade shaft to the spindle bearings, causing:   · Bearing pitting: Small pits form on rolling elements and raceways under micro-impacts, gradually increasing vibration levels. · Cage fracture: High-frequency alternating stress leads to fatigue fracture of the bearing cage. · Spindle bending: Long-term unilateral force causes permanent bending deformation of the spindle. · Blade shaft wear: Fretting wear at the shaft-bearing interface creates clearance.   2. Four Typical Symptoms of Poor Dynamic Balance     1. Spindle vibration levels continuously rise: Vibration velocity (RMS) measured with a vibration meter increases from the normal 1.0mm/s to above 3.0mm/s. 2. Abnormal blade wear: The edge shows "wavy" wear patterns, with circular blades for precision slitting wearing significantly faster in certain areas. 3. Declining product accuracy: Slitting width fluctuations increase, and burrs alternate between large and small. 4. Spindle housing overheating: Increased bearing friction raises the spindle housing temperature by 10-20°C above normal.     3. Common Causes of Poor Dynamic Balance   · Inhomogeneous blade material (segregation, porosity) · Non-concentric inner and outer diameters during grinding (excessive concentricity error) · Cumulative installation errors from shafts, spacers, and nuts · Uneven edge wear after use of stainless steel strip slitting circular blades · Failure to re-balance after resharpening   4. Dynamic Balance Grade Standards and Recommendations     For high-speed slitter blades (line speed > 500m/min), the dynamic balance grade should reach G2.5 or higher. For example, a 200mm diameter, 5kg blade allows a residual unbalance of approximately 0.025g·m at G2.5 — equivalent to an eccentric mass of 0.025g at a 100mm radius (about the weight of two grains of salt).   5. How to Solve Dynamic Balance Problems?     1. Perform dynamic balance correction before shipment   Every high-precision custom blade from Mingbai Technology undergoes single-plane or dual-plane dynamic balance testing before shipment, with residual unbalance better than G2.5 requirements.   2. On-site dynamic balance service   For already installed blades, portable dynamic balancers can perform correction on the equipment without disassembly.   3. Regular testing   It is recommended to test blade dynamic balance every 3-6 months, especially for wear-resistant blades for automotive panel slitting under heavy load conditions.   6. Cost Comparison of Dynamic Balance Problems   · Preventive balancing: approximately 200-500 RMB per blade · Replacing spindle bearings: approximately 5,000-20,000 RMB, with 2-3 days of downtime · Replacing the complete spindle assembly: approximately 30,000-100,000 RMB, with 1-2 weeks of downtime   Conclusion   Slitter blades with poor dynamic balance may only show slightly increased vibration in the short term, but long-term operation will inevitably damage the spindle. Dynamic balance is not an "optional feature," but a "standard safety measure" for high-speed slitting. Mingbai Technology provides dynamic balance inspection reports for every custom slitter blade to give you peace of mind. For on-site dynamic balance services, feel free to contact our technical team. Website: www.mingbaiblade.com
  • When Customizing Blades, Does Requesting "Sample-Based Manufacturing" Actually Cause More Problems?
    Jun 17, 2026
    When customizing custom blades, many customers believe that "sample-based manufacturing" is the safest approach — "I provide an old blade, and you just copy it." However, Mingbai Mechanical Tool Technology Co., Ltd. has found that this seemingly simple request is actually the most prone to problems. Why? Because the old blade itself may already be "lying" to you.   1. Three Things an Old Blade Won't Tell You     1. It has already been resharpened multiple times   A used slitting blade may have been resharpened 3-5 times, with reduced outer diameter, changed edge angle, and enlarged bore. If you copy it as it is, the new blade will be manufactured to "post-wear dimensions" from the start — resulting in oversized clearance and poor cutting quality upon installation.   2. It may already be deformed or have micro-cracks   Precision circular blade after long-term use may have slight warping on its end face (flatness out of tolerance), or invisible micro-cracks. If you only measure the outer contour during copying without checking for deformation, the new blade will inherit these defects.   3. It may be the result of incorrect selection   If the original blade itself had unsuitable material or angles for your working conditions, copying it will only pass on the same mistakes. Alloy blade for silicon steel slitting with an excessively small edge angle that caused frequent chipping will still chip in the copy.   2. Three Most Common Pitfalls in Sample-Based Manufacturing   1. Only measuring dimensions, not asking about working conditions   Some manufacturers simply take measurements without asking about equipment type, material thickness, or cutting speed. The resulting high-speed steel custom blade may have correct dimensions but wrong material or hardness, causing problems upon installation.     2. Ignoring wear compensation   The old blade's outer diameter has shrunk due to resharpening. If the new blade is made to this dimension, the clearance will be too large upon installation, leading to severe burrs. The correct approach is to deduce the original factory outer diameter based on the number of resharpenings during reverse engineering, and manufacture to the original size.       3. Overlooking coating   The old blade's coating may have completely worn away and be invisible to the naked eye. If coating requirements are not specifically stated during sample-based manufacturing, the manufacturer may produce an uncoated blade with only one-third of the original blade's life.   3. How to Properly Execute "Sample-Based Manufacturing"   1. Provide sample + working condition information   In addition to sending old slitter blade samples, provide: material grade, thickness, equipment speed, and current cutting issues (burrs, chipping, short life, etc.).   2. Accept reverse optimization suggestions   Upon receiving the sample, Mingbai Technology will:   · Measure dimensions and angles · Test hardness and metallographic structure · Evaluate whether the original design is reasonable based on working conditions   If the original design has flaws, such as excessively small edge angle on stainless steel strip slitting circular blade, we will proactively propose optimization rather than blindly copying.     3. Prioritize original factory drawings   If original drawings are available, manufacture according to the drawings, using the old sample only as reference. When no drawings exist, Mingbai Technology can generate CAD drawings through reverse engineering and have you confirm them before production.   4. When Is Sample-Based Manufacturing the Best Choice?   · The original blade design has been very successful and has performed stably for years · The original manufacturer has ceased production and cannot provide drawings · The blade has a complex shape that cannot be fully expressed by drawings   5. Mingbai Technology's "Sample-Based Manufacturing" Process   1. Customer sends the old blade with working condition description 2. Mingbai laboratory performs 3D measurement and hardness testing 3. Reverse engineering drawings are issued with recommended optimization items marked 4. Production proceeds after customer confirmation, with first-article inspection before batch delivery 5. The old blade is returned with the shipment     Conclusion   "Sample-based manufacturing" is not simple replication, but "understanding" the usage history behind the old blade. Mingbai Technology does not stop at replication; we aim for optimization — making the new blade more durable and more suitable than the old sample. If you have sample-based manufacturing needs, feel free to contact our technical team. Website: www.mingbaiblade.com
  • Why Do Your Mechanical Blades Break More Easily in Winter Than in Summer?
    Jun 16, 2026
    Many slitting workshops experience a strange phenomenon: the same circular blades and slitter blades work perfectly in summer but break frequently once winter arrives. Some suspect the blade quality has "deteriorated," but Mingbai Mechanical Tool Technology Co., Ltd. tells you: the problem is not the blade, but the temperature. Low winter temperatures change the mechanical behavior of materials, and understanding this principle is key to effective prevention.   1. The Physical Essence of Low-Temperature Fracture   Most mechanical blade materials (high-speed steel, alloy tool steel) have low-temperature brittleness. When the ambient temperature drops below the material's ductile-brittle transition temperature (typically -10°C to 10°C), the impact toughness of the material drops sharply. In summer (above 25°C), the blade can absorb impact energy through plastic deformation; in winter (near 0°C), the same impact energy cannot be dissipated, leading to crack formation and rapid propagation at the edge — this is the direct cause of blade fracture.     2. Three Major Causes of Winter Fracture     1. Increased internal stress due to material contraction   The blade and blade shaft are made of different materials with different coefficients of thermal expansion. In winter, the blade bore contracts, making the fit with the shaft tighter and increasing installation stress. When high-speed slitting circular blades are subjected to lateral forces during operation, the existing stress plus shear stress easily triggers fracture at stress concentration points such as bore keyways or lightening holes.   2. Increased lubricant viscosity, leading to higher impact loads   At low temperatures, lubricating oil becomes thicker, reducing lubrication between the blade and material, and increasing cutting resistance. The impact loads caused by sudden resistance changes are borne by the increasingly brittle edge, causing heavy plate slitting mechanical blades to crack at the moment of engagement.   3. Thermal stress caused by workshop temperature differences   In winter, the morning workshop temperature may be only 5°C, while after high-speed operation, the blade temperature can reach 40-50°C. This rapid heating from a large temperature difference creates thermal stress, which poses a severe test for the microstructure of precision custom blades.   3. Which Blades Are Most Vulnerable in Winter?   · High-hardness alloy blades: The higher the hardness, the higher the ductile-brittle transition temperature, and the greater the sensitivity to low temperatures. · Large-size slitter blades: Larger volume means more internal defects and stress concentration points. · Thin-edge circular blades: The small cross-section of the edge makes impact resistance weaker. · Old blades with long service life: They already have microscopic fatigue cracks, which propagate more easily at low temperatures.   4. Six Measures to Prevent Winter Fracture   1. Preheat the blade: Place the blade in an environment above 20°C for at least 2 hours before installation, or use an induction heater to preheat the blade to 30-40°C.     2. Reduce cutting speed: Lower speed by 10%-15% in winter to reduce impact energy. 3. Switch to low-temperature lubricant: Use synthetic lubricating oils with a high viscosity index to ensure good low-temperature fluidity.     4. Decrease blade gap: Materials become harder in winter, so appropriately reducing the gap can reduce impact. 5. Increase no-load warm-up: Run the machine at no load for 5-10 minutes before starting to gradually warm the blade. 6. Inspect upon receipt: For custom slitter blades received in winter, do not install immediately; let them sit for 24 hours to acclimate to room temperature.   5. After Fracture Occurs   · If the fracture surface has a fine porcelain-like appearance, it indicates low-temperature brittle fracture. Adjusting the environment is sufficient. · If the fracture surface shows old crack marks, the blade already had fatigue damage. Increased non-destructive inspection is needed. · For batch fractures, check the low-temperature impact toughness of the material. Mingbai Technology can provide low-temperature impact testing services for stainless steel strip slitting circular blades.     6. Mingbai Technology's Winter Protection Solutions   Mingbai Mechanical Tool Technology Co., Ltd. has introduced low-temperature tough alloy blades specifically for winter use. By adjusting the tempering temperature in the heat treatment process, we improve low-temperature toughness while maintaining hardness. We also provide blade preheating devices and low-temperature lubricant solutions to help customers get through winter smoothly.     Conclusion   Winter blade fractures are not a quality issue, but a temperature issue. Understanding low-temperature brittleness, preheating properly, adjusting parameters, and selecting suitable blade materials can all prevent fractures. Mingbai Technology is willing to provide specialized guidance for winter blade use. Website: www.mingbaiblade.com
  • Circular Blade Bore Keyway Wear: Repair or Scrap the Entire Blade?
    Jun 15, 2026
    In slitting equipment, circular blades transmit torque through the bore keyway to the blade shaft. After long-term use, the keyway side walls experience wear, plastic deformation, and even cracks due to repeated impact. Faced with this situation, many users directly scrap the blade, causing waste; others continue to use it reluctantly, leading to equipment damage. Mingbai Mechanical Tool Technology Co., Ltd. provides you with judgment criteria and repair solutions.   1. Three Typical Forms of Keyway Wear   · Light wear: Keyway side wall width increase < 0.1mm, no deformation, no cracks. The blade still has slight play after installation. · Moderate wear: Width increase of 0.1-0.3mm, indentation or slight curling at keyway edges. The blade wobbles periodically during operation. · Severe wear: Width increase > 0.3mm, cracking or chipping at keyway edges. The blade is obviously eccentric after installation and cannot slit properly.     2. Repair or Scrap? Judgment Criteria   Low-speed slitting heavy-duty circular blades: If the keyway wear is light (width increase < 0.1mm) and the blade still has multiple resharpening allowances left, repair is recommended. The repair cost is about 15%-25% of a new blade.   High-speed slitting precision alloy blades: Due to the high dynamic balance requirement for high-speed operation, moderate wear (>0.2mm) is recommended to be scrapped directly to avoid instability after repair causing equipment accidents.   Stainless steel strip slitting wear-resistant circular blades: If the keyway wear is on one side, repair by overlay welding and re-milling is possible; if both sides are worn or cracks appear, scrap the blade.   3. Detailed Repair Methods   1. Overlay welding + re-milling (suitable for high-speed steel blades)   · Use nickel-based or cobalt-based welding rods to build up the worn keyway side wall. · Perform stress relief annealing after welding. · Re-machine the keyway on a milling machine according to the original dimensions, width tolerance +0.02/+0.05mm. · Suitable for automotive panel slitting custom blades.     2. Bush sleeve method (suitable for blades with larger bores)   · Bore out the original bore by 1-2mm and press in a heat-treated inner sleeve. · Machine a new keyway on the inner sleeve, offset by a certain angle from the original keyway position. · Suitable for thick plate slitting mechanical blades.   3. Custom non-standard key (emergency treatment)   · Measure the actual keyway width after wear and customize an oversized key (non-standard size). · Only for temporary use, recommended not to exceed 200 hours. · Suitable for emergency use on battery electrode slitting ultra-thin circular blades.   4. Situations Where Repair Is Not Recommended   · The keyway edge already has cracks (even if very short). · The blade has been resharpened more than 5 times, and the remaining thickness is insufficient. · The bore has become out-of-round, and concentricity exceeds >0.03mm. · For small-sized circular blades with low unit purchase cost, direct replacement is more economical.   5. Verification After Repair   A repaired precision mechanical blade must pass the following inspections before installation:   1. Keyway width, depth, and position meet drawing requirements. 2. Bore roundness ≤ 0.005mm. 3. Blade end face flatness ≤ 0.003mm. 4. Radial runout after shaft mounting ≤ 0.01mm.     6. Mingbai Technology's Repair Services   Mingbai Mechanical Tool Technology Co., Ltd. provides circular blade bore keyway wear repair services, including overlay welding, annealing, precision milling, and inspection. We can provide keyway repair solutions for lithium battery electrode slitting carbide blades. We also accept old blade recycling evaluations and provide free repair or scrap recommendations.     Conclusion   Keyway wear in circular blade bores does not mean the entire blade is scrap. Light wear can be repaired by overlay welding; moderate wear requires careful evaluation; severe wear or blades with cracks should be decisively scrapped. Mingbai Technology is willing to use its professional repair techniques to help you extend blade life and reduce tooling costs. Website: www.mingbaiblade.com
  • After Mechanical Blades Become Soft Due to Annealing, Is There Any Way to Re-Harden Them?
    Jun 10, 2026
    In slitting production, slitter blades or circular blades often undergo "annealing" due to excessive friction heat, dry cutting, or overheating during resharpening — the edge becomes locally soft and hardness drops. Many users think the blade is scrap and can only be thrown away. Mingbai Mechanical Tool Technology Co., Ltd. tells you: in some cases, re-hardening is possible, but certain conditions must be met.   1. How Does Annealing Happen?   Annealing occurs when the blade edge temperature exceeds the material's tempering temperature (approx. 550-600°C for high-speed steel, above 800°C for carbide), causing decomposition of the martensitic structure, precipitation of carbides, and a sharp drop in hardness. Common causes include:   · High-speed dry cutting of stainless steel or high-strength steel, with heat buildup from friction · Dull grinding wheel or excessive feed rate during resharpening, resulting in grinding-burned annealed mechanical blades · Interruption of lubrication and cooling, causing dry friction between blade and material     2. Can Annealed Blades Be Re-Hardened?   The answer is: it depends.   · High-speed steel blades: They can be re-quenched and tempered to restore original hardness. However, the blade may deform, and the surface decarburized layer must be removed. · Carbide blades: Cannot be restored to hardness by conventional heat treatment. The substrate has undergone irreversible phase transformation. · Stainless steel blades: Some precipitation-hardening stainless steels can be re-solution treated and aged, but martensitic stainless steels require re-quenching after annealing.     3. Methods and Limitations of Re-Hardening   1. Re-heat treatment process suitable for high-speed steel blades   Annealed high-speed steel slitter blades can undergo:   · Annealing softening (to eliminate the original structure) · Re-quenching (1180-1240°C oil or gas quenching) · 3-4 tempering cycles (550-560°C)   This can restore original hardness of HRC63-65. However, the blade may deform by 0.05-0.1mm, requiring subsequent precision grinding.     2. Local quenching method   For local edge annealing of circular blades, flame or high-frequency induction local heating quenching can be used to harden only the edge area, avoiding overall deformation. This method is suitable for precision circular blades for thin sheet slitting.     3. Coating as an alternative   If the annealing depth is very shallow (<0.02mm) and the blade has no remaining resharpening allowance, PVD coating can be tried. The coating itself has high hardness (>HRC80) and can temporarily "mask" the softness, but the substrate is soft and impact resistance is poor. Ultra-thin alloy blades for battery electrode slitting may consider this option.   4. Precautions After Re-Hardening   · The edge must be precision ground to remove the oxidation and decarburization layer. · Flatness and concentricity must be re-inspected; straightening is necessary if needed. · The life of a re-hardened blade is typically lower than that of a new original blade (about 70%-85%).     5. When Is Re-Hardening Not Worthwhile?   · Blade thickness has been reduced due to multiple resharpenings, remaining effective thickness < 60% of original. · The blade has cracks or severe deformation. · Annealing depth > 0.5mm, requiring a large number grinding. · For small-sized blades with low procurement cost, direct replacement is more economical.   6. Mingbai Technology's Recommendations   Mingbai Mechanical Tool Technology Co., Ltd. recommends customers to:   · Avoid annealing: Use sufficient lubrication and cooling, control resharpening parameters. · Inspect after annealing: Use a portable hardness tester to confirm the annealed area and depth. · Professional factory treatment: If re-hardening is needed, send back to Mingbai for vacuum heat treatment. We provide annealing repair service for high-speed steel circular blades for stainless steel strip slitting. · Evaluate economics: We will help you calculate repair cost vs. replacement cost for free.     Conclusion   Annealed mechanical blades are not necessarily scrap. High-speed steel blades can be re-heat treated to restore hardness, but the risks of deformation and economics must be weighed. Carbide and stainless steel blades need case-by-case analysis. Mingbai Technology is willing to provide inspection and repair recommendations for annealed blades, helping every blade fulfill its potential. Website: www.mingbaiblade.com
  • How to Use Simple Methods to Determine if Newly Purchased Circular Blades Have Been Precision Ground?
    Jun 09, 2026
    When purchasing new circular blades, the worst fear is encountering inferior products that look shiny on the surface but cause constant burrs and halve the blade life once installed. Blades that have truly undergone precision grinding have identifiable microscopic characteristics on their edges and surfaces. Mingbai Mechanical Tool Technology Co., Ltd. teaches you several quick methods to judge without professional instruments.   1. Look: Observe the edge with the naked eye or a magnifying glass   High-precision circular blades for precision slitting – after precision grinding, the edge will show a uniform, non-reflective "dark line" (actually a very small edge land) about 0.05-0.1mm wide. In contrast, ordinary ground blades often have visible burrs, chipping, or local reflective spots on the edge.     2. Feel: Lightly scrape the sides of the edge with a fingernail or the back of a finger   Polished circular blades for mirror-grade surface finishing – after precision grinding, both sides of the edge are as smooth as a mirror, and a fingernail glides without roughness. Rough ground blades have microscopic grooves, and the fingernail will feel resistance. Use the back of a finger to avoid cuts.     3. Shine: Side-illuminate the surface reflection with a strong light   Wear-resistant circular blades for stainless steel strip cutting – after precision grinding, the reflected image on the surface is clear and undistorted; ordinary ground surfaces cause the reflected lamp tube image to distort and blur. Qualified blades show uniform reflected light and a clear lamp tube edge.     4. Measure: Quickly verify with a feeler gauge or dial indicator   Alloy blades for high-hardness alloy materials – place the blade flat on a clean granite surface plate or glass plate, and try to insert a 0.02mm feeler gauge between the blade and the plate. If the gauge can be inserted more than 5mm, flatness is poor. Then use a micrometer to measure thickness at different positions on the blade edge; the difference should be ≤0.005mm.     5. Test: Listen to the no-load rotation after installation   Slitter blades for high-speed slitting – install the blade on the equipment, rotate manually or at low speed, and listen with a screwdriver handle pressed against your ear. A precision ground blade runs with a steady, continuous sound; a blade with runout or grinding defects will produce a periodic "swish-swish" sound.     6. Compare: Use a known qualified blade as a reference   Ultra-thin circular blades for food packaging film slitting – if you have a blade that has been performing well, place it side by side with the new blade under a strong light and compare the edge reflection. The width of the dark line on a qualified new blade should be similar to that of the reference blade.     Mingbai Technology's Quality Commitment   Every custom blade and stainless steel blade produced by Mingbai Mechanical Tool Technology Co., Ltd. undergoes precision grinding on five-axis CNC grinders and 100% edge inspection before shipment. We guarantee edge roughness Ra ≤ 0.2μm, flatness ≤ 0.002mm (within 200mm diameter), and edge land width controlled between 0.03-0.08mm (adjusted according to material).   Conclusion   Determining whether circular blades have been precision ground does not require complex instruments. Look at the edge dark line, feel the surface smoothness, shine for reflection clarity, measure flatness and parallelism, listen to the no-load sound, and compare with a reference sample. Master these six techniques, and you will easily identify high-quality blades. Mingbai Technology is willing to be your reliable blade supplier. Website: www.mingbaiblade.com
  • When Slitter Blades Produce Wavy Edges, Is the Problem with the Blade or the Equipment?
    Jun 08, 2026
    In metal slitting operations, wavy edges (also known as "scalloped edges" or "snake bends") on the material slit by slitter blades are among the most difficult defects to troubleshoot. Many users first suspect blade quality, but Mingbai Mechanical Tool Technology Co., Ltd., based on hundreds of on-site diagnoses, has found that about 60% of wavy edge problems originate from the equipment, and only 40% are directly related to the blade. This article helps you quickly identify the root cause and provides blade selection recommendations for different working conditions.   1. Two Typical Types of Wavy Edges   · High-frequency fine wavy edges: The distance between peaks and valleys is small (5-20mm), usually related to the rotational frequency of the blade or blade shaft. · Low-frequency large wavy edges: The distance between peaks and valleys is large (50-200mm), usually related to equipment vibration, tension fluctuations, or the material itself.     2. First, Inspect the Equipment: Three Most Problematic Areas   1. Excessive clearance in blade shaft bearings   When bearings are worn, the blade experiences radial movement under shearing forces, causing the edge trajectory to become elliptical or oscillating, producing wavy edges. Inspection method: stop the machine, use a dial indicator against the outer diameter of the blade shaft, and pry up and down. If the clearance > 0.02mm, the bearings need replacement.     2. Poor parallelism between upper and lower blade shafts   Non-parallel shafts cause the blade gap to vary along the axial direction, resulting in uneven local stress on the material and producing wavy edges. Inspection method: measure the gap between upper and lower blades at both ends of the shaft with a feeler gauge. If the difference > 0.02mm per meter, adjustment is needed.     3. Insufficient rigidity of the equipment base or blade holder   During high-speed slitting, resonance between the blade holder vibration frequency and the blade shaft rotational frequency can also produce wavy edges. Try changing the cutting speed by 10%-15%. If the wavy edges disappear or shift position, the problem is equipment resonance.   3. Blade-Related Problems: Inspection Priorities for Different Scenarios   If equipment inspection reveals no issues, wavy edges may stem from blade precision or incorrect selection. Below are common blade problems in different slitting scenarios:   High-hardness circular blades for stainless steel strip slitting: If roundness > 0.005mm, radial runout occurs with each revolution, producing evenly spaced wavy edges. Use a roundness tester; if out of tolerance, send back for resharpening or replacement. Mingbai Technology offers such blades with roundness controlled within 0.003mm.     Wear-resistant alloy blades for silicon steel slitting: End face flatness should be ≤ 0.003mm. Excessive flatness causes axial runout, producing fine wavy edges. Place the blade on a granite surface plate and check with a feeler gauge. For silicon steel slitting in new energy vehicle motors, choose precision-grade blades with higher flatness.     Stainless steel blades for aluminum strip cutting: The clearance between the blade bore and the blade shaft should be ≤ 0.02mm. Excessive clearance causes eccentric installation, generating periodic radial impact during rotation and forming wavy edges. Mingbai Technology's Anti-adhesion circular blades designed for aluminum strip slitting use mirror polishing to reduce wavy edges.   Ultra-thin mechanical blades for composite film slitting: Hardness uniformity is critical. If heat treatment hardness deviation exceeds ±2 HRC, local edge wear rates differ, producing irregular wavy edges. Use a hardness tester for multi-point inspection. Mingbai's High-precision film slitting circular blades undergo 100% hardness inspection per batch.   Carbide blades for battery electrode slitting: Microscopic edge nicks can also induce wavy edges. It is recommended to use Lithium electrode dedicated circular blades, which are inspected under 200x magnification for edge integrity before shipment.   Custom slitter blades for automotive panel slitting: Uneven coating thickness can cause local friction coefficient variations, leading to wavy edges. Mingbai Technology provides Automotive steel dedicated slitter blades with PVD coating uniformity controlled within ±0.5μm.   4. Quick Judgment Flow Chart   1. First inspect the equipment: bearing clearance, blade shaft parallelism, blade holder rigidity. 2. Then inspect the blade: roundness, flatness, bore fit, hardness uniformity, coating quality. 3. Exchange test: move the suspected blade to another normal machine and run it.    · If wavy edges disappear → problem with the original equipment.    · If wavy edges persist → problem with the blade.   5. Mingbai Technology's Solutions   Mingbai Mechanical Tool Technology Co., Ltd. provides one-stop services for slitter blade wavy edge diagnosis:   · Free on-site inspection of blade roundness, flatness, and hardness. · Assistance in troubleshooting equipment bearing clearance and parallelism. · Supply of high-precision custom slitter blades with roundness ≤ 0.003mm and flatness ≤ 0.002mm. · Dedicated blade selection recommendations for different materials (stainless steel, silicon steel, aluminum strip, composite film, battery electrodes, automotive panels).     6. Case Study   A stainless steel strip slitting plant used high-hardness circular blades for stainless steel strip slitting but still experienced wavy edges. Mingbai engineers inspected on-site and found that the radial clearance of the lower blade shaft bearing was 0.08mm (standard ≤ 0.02mm). After bearing replacement, the wavy edges completely disappeared.   Conclusion   When slitter blades produce wavy edges, do not focus only on the blade. First check the equipment's bearings, parallelism, and rigidity, then confirm whether the blade is suitable for your specific material. Mingbai Technology provides dedicated blades for different slitting scenarios, ensuring more accurate selection and smoother cutting. https://www.mingbaiblade.com/
  • Can I Only Provide an Old Blade Sample for Custom Blades? What Should I Pay Attention To?
    Jun 03, 2026
    Many customers, when needing to reorder custom blades, only have a worn old blade on hand and no original drawing. They often ask: can I only provide an old blade sample for an exact replication? The answer is: yes, but there are several key details to pay attention to. Mingbai Mechanical Tool Technology Co., Ltd., based on numerous "sample-based customization" cases, outlines the operational points and precautions for you.   1. Providing Only an Old Blade Sample Is Feasible   As long as the old blade is not severely deformed, chipped, or corroded, Mingbai Technology can use reverse engineering measurement technology to accurately restore its geometric dimensions and edge parameters. We use coordinate measuring machines and profilometers to capture key feature points of the blade and generate manufacturing drawings. This method is particularly suitable for reproduction of old blades without drawings, saving customers the trouble of re-measuring themselves.     2. Six Details to Pay Attention to When Providing an Old Blade Sample   1. Confirm whether the sample is representative   If you have multiple old blades of the same specification, it is recommended to choose the one with the least wear and no obvious deformation as the sample. Choosing the sample with the least wear improves reverse engineering accuracy. If all blades are severely worn or chipped, it is better to provide a new blade sample or contact the original manufacturer for drawings.   2. Clean the sample surface     Before sending, be sure to thoroughly clean the surface of the old blade with alcohol or cleaner to remove oil, rust, and adhered material. Residual dirt will affect measurement accuracy, especially for small features on the edge area.     3. Mark the edge direction and mounting surface   Use a marker pen or label to mark the edge direction and mounting surface on the old blade to avoid confusing the front and back during reverse engineering. For circular blades or slitter blades with asymmetrical edges, this is especially important.     4. Provide supplementary operating condition information   Relying only on the old blade sample, the manufacturer cannot know the material, thickness, equipment type, etc. It is recommended that you provide the grade and thickness of the material being slit, as well as the equipment speed and tension range. This information helps Mingbai engineers determine whether the original blade design was reasonable and optimize parameters if necessary.   5. Indicate whether you accept optimization suggestions   The design of an old blade may not be optimal. Mingbai Technology may propose edge angle or coating optimization solutions based on your operating conditions. If you want an exact 1:1 replica, you must clearly state this; if you are willing to accept optimization, please also indicate that.   6. Package with shock and damage protection   The old blade itself may have fragile chipped areas. When sending, it should be individually wrapped with foam or air cushion bags to avoid secondary damage from collisions during transport.   3. Standard Process for Reverse Engineering Customization   Step 1: Customer sends the old blade sample, along with operating condition descriptions and replication requirements. Step 2: Mingbai laboratory performs 3D scanning or coordinate measurement to generate CAD drawings.     Step 3: Confirm drawing parameters (outer diameter, bore, thickness, edge angle, etc.) with the customer. Step 4: Produce according to the drawings, conduct first-article inspection, then deliver in batches. Step 5: Return the old blade sample with the shipment.   4. Situations Where Providing Only a Sample Is Not Suitable   · The blade is severely deformed (flatness > 0.1mm) · The edge has large-area chipping (> 1mm) · The blade surface is severely corroded with lost features · The original blade design itself is unreasonable (e.g., wrong material, angle too small)   In the above cases, it is recommended that Mingbai engineers redesign rather than blindly copy.   5. Mingbai Technology's Advantages in Reverse Engineering Customization   Mingbai Mechanical Tool Technology Co., Ltd. has high-precision coordinate measuring machines and profilometers capable of reverse engineering of complex special-shaped blades with accuracy up to ±0.002mm. We promise:   · 1:1 replication, dimensions perfectly matched · Free drawing confirmation provided · Old blade samples properly kept and returned · Support for material upgrades (e.g., upgrading ordinary steel to alloy blades or stainless steel blades)     6. Customer Case   A packaging machinery factory ran out of circular blades for film cutting because the original manufacturer had discontinued production. The customer sent a worn old blade. Mingbai Technology performed reverse engineering and produced 50 blades. After installation, the cutting performance was exactly the same as the original, solving the customer's urgent problem.   Conclusion   Providing only an old blade sample to customize custom blades is completely feasible, but you need to pay attention to six details: sample selection, cleaning, marking, and information supplementation. Mingbai Mechanical Tool Technology Co., Ltd. is willing to use its professional reverse engineering technology to help you solve the problem of "having a sample but no drawing." Website: www.mingbaiblade.com
1 2 3 4 5 6 7 8
Leave A Message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
submit

leave a message

leave a message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
submit

home

products

WhatsApp

Contact Us