Home

Blog

Blog

  • Abnormal Blade Wear in Silicon Steel Slitting — Is It a Hardness Problem or a Coating Problem?
    Aug 11, 2026
    In silicon steel strip slitting operations, abnormal blade wear is a persistent problem troubling many users. Excessive edge wear leads to frequent downtime for blade changes, affecting production efficiency and directly increasing tooling costs. Faced with wear, many users instinctively think "hardness is insufficient," but after switching to higher hardness blades, the wear persists. Others suspect the coating, yet trying different coatings also shows no improvement. Mingbai Mechanical Tool Technology Co., Ltd., combining the material characteristics of silicon steel slitting and years of field experience, systematically analyzes: is the root cause of abnormal wear hardness or coating?   1. Silicon Steel — The Blade's "Natural Abrasive"   Silicon steel (electrical steel) typically contains 0.5%-4.5% silicon, which exists in the form of solid solutions and silicides. These hard particles generate severe abrasive wear on the cutting edge during shearing, with abrasiveness far higher than ordinary low-carbon steel. At the same time, silicon steel is hard and brittle, requiring the cutting edge to withstand both abrasive cutting and impact loads during shearing — presenting a dual challenge of hardness and toughness for the blade.     2. Insufficient Hardness: Rapid Wear, Edge Quickly Rounds   When blade hardness is lower than the hard phases in silicon steel, the edge is "cut" by silicide particles during shearing, manifesting as:   · Rapid edge rounding (arc-shaped wear land under microscope) · Gradually increasing burrs on the cut edge · Significantly shortened blade change intervals   Test data shows: when slitting the same silicon steel, a blade with HRC58 hardness has a life only 50%-60% of a blade with HRC62 hardness. Therefore, increasing blade hardness is a direct means of extending life.   However, higher hardness is not always better. When hardness exceeds HRC64, blade toughness drops sharply, making it prone to chipping under the brittle impact of silicon steel, actually shortening life.   3. Insufficient Coating: Increased Friction, Adhesion Accelerates Wear   The role of coating in silicon steel slitting is often underestimated. During silicon steel shearing, intense friction occurs between the cutting edge and the material, with localized temperatures reaching 400-600°C. When uncoated or with insufficient coating performance:   · The blade substrate softens at high temperatures, accelerating wear · Silicon in the silicon steel adheres to the blade surface, creating a "cold welding" effect · Adhered material detaches and takes edge material with it, worsening wear   High-quality PVD coatings (such as TiAlN, AlCrN) form a high-temperature-resistant, low-friction protective layer on the edge surface, significantly reducing abrasive and adhesive wear.     4. Hardness vs. Coating: How to Determine the Main Cause?   Silicon steel wear-resistant blades: if the edge shows uniform rounding with gradually increasing burrs and no chipping or adhesion, the main cause is insufficient hardness, and blade hardness should be prioritized for improvement.   If the edge shows small chipping in a peeling pattern, this indicates excessive hardness leading to insufficient toughness, and hardness should be appropriately reduced or heat treatment optimized.   If the edge surface has obvious adhered material (built-up edge) or groove-shaped wear, this indicates insufficient coating or incorrect coating selection, and coating should be added or the coating type changed.   If the edge surface shows peeling marks with exposed grinding lines, this indicates poor coating adhesion or coating peeling, and the coating process should be optimized or the coating solution changed.   If multiple wear patterns appear mixed, both hardness and coating need optimization, requiring systematic adjustment of material and coating combinations.     5. Optimal Combination Solution for Silicon Steel Slitting Blades   Mingbai Technology recommends the following combination:   Powder high-speed steel blades (such as ASP2053, ASP2060) can achieve hardness HRC64-67 with fine and uniform carbides, combining high hardness and good toughness, suitable for silicon steel slitting.   Ultra-fine grain carbide blades with hardness HRA90-93 offer excellent wear resistance, suitable for high-speed slitting scenarios.   For coating selection, TiAlN coated blades withstand 800°C with high hardness, suitable for medium-to-high speed slitting; AlCrN coated blades withstand 1000°C with better anti-adhesion performance than TiAlN, suitable for high-load conditions. Coating thickness should be controlled at 2-4μm; excessive thickness affects edge sharpness.   For edge treatment, micro-passivation is recommended with edge radius R=0.005-0.010mm to eliminate microscopic defects and prevent chipping.   6. Further Investigation of Coating Issues   Sometimes blade hardness meets the standard and the coating is TiAlN, but wear remains severe. In such cases, the following should be investigated:   · Insufficient coating adhesion, peeling during shearing · Uneven coating thickness, locally too thin losing protective effect · Improper pre-coating treatment, edge surface not adequately cleaned affecting adhesion · Coating selection mismatch with working conditions, such as using high-hardness but insufficient toughness coating for low-speed heavy cutting   7. Mingbai Technology's Diagnostic Services   Mingbai Mechanical Tool Technology Co., Ltd. offers silicon steel blade wear diagnosis services:   · Microscope analysis of edge wear morphology (rounding/chipping/adhesion/peeling) · Hardness testing to confirm compliance · Coating adhesion and thickness testing · Comprehensive diagnostic report and optimization recommendations     Conclusion   In silicon steel slitting, abnormal blade wear often involves both hardness and coating issues. Insufficient hardness leads to rapid rounding; insufficient coating leads to adhesion and peeling. By systematically analyzing wear morphology, the main cause can be precisely identified, and targeted optimization measures can be implemented. Mingbai Technology is ready to help you overcome silicon steel slitting wear challenges with professional diagnosis and customized solutions.   FAQ Module:   Q1: What hardness is most suitable for silicon steel slitting blades? A: Recommended hardness is HRC62-64. Below HRC62, wear is rapid; above HRC64, toughness is insufficient and chipping occurs. Powder high-speed steel (ASP2053/ASP2060) offers the best overall performance in this hardness range.   Q2: What is the difference between TiAlN and AlCrN coatings, and how to choose? A: TiAlN withstands 800°C, suitable for medium-to-high speed slitting. AlCrN withstands 1000°C with better anti-adhesion performance, suitable for high-load conditions or silicon steel with silicon content >3%. For conventional conditions, TiAlN is sufficient; for harsh conditions, AlCrN is recommended.   Q3: Why does wear remain rapid even after switching to higher hardness blades? A: There are three possible reasons: insufficient coating causing substrate softening at high temperatures; poor coating adhesion leading to peeling during shearing; or improper edge treatment leaving microscopic defects. A wear morphology analysis is recommended to precisely identify the cause.   Q4: Can coated blades be repeatedly resharpened? Is the coating still effective after resharpening? A: Yes, they can be resharpened. However, the coating at the edge is removed after resharpening, exposing the substrate. It is recommended to recoat after resharpening, or use a blade solution that allows multiple recoating. Mingbai Technology offers one-stop resharpening + recoating services.   Q5: How often should silicon steel slitting blades be replaced? A: There is no universal standard; it depends on silicon content, slitting speed, equipment precision, and other factors. It is recommended to use the "burr height method": schedule resharpening when burrs exceed 0.05mm, and replace with new blades when burrs exceed 0.10mm. Regularly record blade change intervals to establish your own life standards. Website: www.mingbaiblade.com
  • Severe Blade Sticking When Slitting Soft Materials Like Copper and Aluminum — Which Alloy Blade Grade Is Most Suitable?
    Aug 10, 2026
    In the slitting of soft materials such as copper strips, aluminum strips, copper foil, and aluminum foil, "blade sticking" is one of the most frustrating issues for operators. Material adhering to the cutting edge forms a built-up edge (BUE), which at best causes burrs and surface scratching, and at worst leads to chipping, strip breakage, and frequent downtime for cleaning. Many operators try adjusting speed or increasing cooling, but with limited effect — the root cause often lies in a mismatch between the blade material grade and the characteristics of the soft material. Mingbai Mechanical Tool Technology Co., Ltd., combining materials science and slitting experience, explains the sticking mechanism in copper and aluminum slitting and recommends the most suitable carbide blade grades.   1. Why Do Soft Materials Like Copper and Aluminum Stick to Blades?   Copper, aluminum, and their alloys are characterized by low hardness, high ductility, and high adhesion. During slitting, intense squeezing and friction occur between the cutting edge and the material, causing localized temperature rise. Under high temperature and pressure, metal particles from the soft material undergo a "cold welding" effect with the blade surface, gradually adhering and accumulating to form a built-up edge. Once formed, the built-up edge alters the edge geometry, increasing cutting resistance and further raising temperature — creating a vicious cycle.   Moreover, copper and aluminum have good thermal conductivity, so heat rapidly transfers from the cutting zone to the entire blade, accelerating edge softening and further reducing anti-adhesion capability. Therefore, to solve the sticking problem, the blade's material, grain size, hardness, and surface condition are all indispensable.     2. Core Logic for Selecting Alloy Blade Grades   Carbide blades are classified into YG (tungsten-cobalt), YT (tungsten-titanium), YW (universal), and other grades. For non-ferrous metals like copper and aluminum, YG grades are the first choice. YG alloys use tungsten carbide (WC) as the hard phase and cobalt (Co) as the binder, offering excellent impact resistance and toughness, making them suitable for machining non-ferrous metals that produce short chips.   The numbers in the grade designation (e.g., YG6X, YG8, YG15) indicate the approximate percentage of cobalt content — higher cobalt content means better toughness and impact resistance, but slightly lower hardness and wear resistance. Thus, selecting the right grade requires balancing anti-adhesion (high hardness) with anti-chipping (high toughness).   3. Recommended Grades and Applicable Scenarios     3.1 YG6X — First choice for precision slitting of thin materials   YG6X is a fine-grain carbide with high hardness (HRA91-91.5) and good wear resistance, with a cobalt content of about 6%. The fine-grain structure ensures more uniform carbide distribution, allowing the edge to be ground sharper for lower cutting resistance, making it ideal for thin copper strips, thin aluminum strips, copper foil, and aluminum foil in high-precision slitting. For soft materials under 0.5mm thickness, YG6X effectively reduces extrusion deformation and adhesion. Thin material precision slitting blades are the ideal choice for such conditions. However, due to its relatively moderate toughness, YG6X is not suitable for heavy rough cutting with impact loads.   3.2 YG8 — The "all-rounder" balancing wear resistance and toughness   YG8 has a cobalt content of about 8%, hardness HRA89-89.5, and higher transverse rupture strength than YG6X. It is one of the most widely used grades in copper and aluminum slitting, suitable for conventional thickness copper and aluminum strips (0.5-3mm) as well as aluminum foil and copper foil. YG8 achieves a good balance between wear resistance and impact resistance, maintaining edge sharpness while withstanding moderate impact loads — making it a "safe choice" for most copper and aluminum slitting applications.   3.3 YG15 — First choice for thick materials, rough cutting, and high-impact conditions   YG15 has a cobalt content of about 15%, hardness HRA87-89, with high transverse rupture strength and excellent toughness. It is suitable for thick copper plates, thick aluminum plates (>3mm) and rough cutting applications with joints or large thickness fluctuations. The higher cobalt content makes the blade less prone to chipping under impact, making it suitable for roughing where surface finish is not critical. Thick copper plate rough cutting blades perform excellently in such conditions. However, wear resistance is slightly lower than YG6X and YG8, so it is not suitable for ultra-thin precision slitting.   3.4 Ultra-fine grain carbide — An upgrade choice for high-end precision slitting   For high-precision slitting of ultra-thin copper foil, aluminum foil (<0.1mm) or lithium battery electrodes, conventional YG grades may not be ideal. Ultra-fine grain carbide (grain size ≤ 0.5μm) can achieve hardness of HRA90-93 and transverse rupture strength > 4000N/mm², with a service life 5-10 times that of conventional carbide. This material maintains extremely high hardness while improving edge toughness, making it especially suitable for high-precision burr-free slitting of ultra-thin soft materials.     4. Synergistic Optimization of Edge Parameters and Coatings   Choosing the right grade is only the first step; edge parameters and coating selection are equally critical.   · Edge angle: For soft materials like copper and aluminum, a smaller edge angle (20°-25°) is recommended to reduce cutting resistance and extrusion deformation. A dull edge exacerbates friction and adhesion.     · Edge surface finish: The smoother the edge surface, the harder it is for material to adhere. Polishing to Ra ≤ 0.1μm combined with a sharp rake angle design is recommended. · Coating selection: In most cases, uncoated carbide or special anti-adhesion coatings can be used for copper and aluminum. TiAlN (purple-black) coatings offer excellent anti-adhesion performance, suitable for high-speed slitting; DLC (diamond-like carbon) coatings have an extremely low friction coefficient (as low as 0.1), effectively inhibiting BUE formation. For ultra-thin aluminum foil, some applications even recommend no coating to avoid compromising edge sharpness due to coating thickness. Anti-adhesion coated blades are highly effective in soft material slitting.     5. Supporting Process Recommendations   · Cooling and lubrication: For copper and aluminum slitting, oil mist lubrication or minimum quantity lubrication (MQL) is recommended, with a flow rate of 10-20 ml/h to effectively reduce friction temperature and adhesion risk. · Regular inspection: Inspect the edge every shift; if early signs of BUE are found, clean promptly. · Speed control: Recommended slitting speed for copper and aluminum: 80-150 m/min. Excessively high speed increases friction heat; too low speed increases material dwell time at the edge.   6. Mingbai Technology's Copper and Aluminum Slitting Blade Solutions   Mingbai Mechanical Tool Technology Co., Ltd. offers a dedicated blade series for slitting soft materials like copper and aluminum:   · Copper-aluminum slitting circular blades: Available in YG6X, YG8, YG15, and ultra-fine grain grades, precisely matched to working conditions. · Mirror-polished copper-aluminum blades: Edge Ra ≤ 0.05μm, effectively reducing adhesion. · Optional TiAlN/DLC anti-adhesion coatings. · Material selection recommendations and on-site working condition diagnosis services.     7. Case Study   A copper strip slitting plant used conventional carbide blades for 0.2mm copper foil. Severe sticking occurred every 2 hours, requiring frequent cleaning. After switching to Mingbai Technology's ultra-thin copper foil slitting blades (ultra-fine grain YG6X + mirror polishing), the sticking interval extended to 8 hours, and blade life increased by 3 times.   Conclusion   Severe blade sticking when slitting soft materials like copper and aluminum originates from a mismatch between blade material and material characteristics. For thin precision slitting, choose YG6X or ultra-fine grain alloy; for conventional thickness, choose YG8; for thick rough cutting, choose YG15. Combined with appropriate edge angles, high surface finish, and anti-adhesion coatings, the sticking problem can be effectively controlled. Mingbai Technology is ready to help you eliminate sticking issues with professional material solutions.   FAQ Module:   Q1: Why can't ordinary high-speed steel blades be used for copper and aluminum slitting? A: High-speed steel hardness (HRC58-62) is far lower than carbide (HRA89-93). In copper and aluminum slitting, the edge wears quickly, becomes dull, and increased friction worsens sticking. Carbide's hardness and anti-adhesion performance are far superior, making it the preferred material for copper and aluminum slitting.   Q2: Which is better for cutting 0.3mm copper strip, YG6X or YG8? A: YG6X is recommended. 0.3mm is thin material precision slitting. YG6X has higher hardness and finer grain, allowing a sharper edge with lower cutting resistance, reducing extrusion deformation and adhesion risk. YG8 has better toughness but lower hardness, making it more suitable for medium thickness or applications with some impact.   Q3: Are coated blades really effective in copper and aluminum slitting? A: Yes. TiAlN or DLC coatings significantly reduce the friction coefficient and material adhesion. DLC coatings can achieve a friction coefficient as low as 0.1, effectively inhibiting BUE formation. However, for ultra-thin aluminum foil slitting, coatings are sometimes not recommended as the coating thickness may affect edge sharpness; this should be evaluated based on specific working conditions.   Q4: What should the blade gap be for copper and aluminum slitting? A: For soft copper and aluminum materials, the recommended gap is 4%-6% of material thickness. Too small a gap exacerbates extrusion and adhesion; too large a gap causes tearing burrs. Use the lower limit (4%) for thin materials and the upper limit (6%) for thick materials, with fine-tuning through trial cuts.   Q5: How much more expensive are ultra-fine grain carbide blades compared to conventional YG grades? Is it worth it? A: Ultra-fine grain carbide typically costs 2-3 times more than conventional YG grades, but its service life can be 5-10 times longer. For high-precision slitting of ultra-thin copper foil, aluminum foil, or lithium battery electrodes, the overall cost of use is actually lower, making it highly worthwhile. Website: www.mingbaiblade.com
  • Food-Grade Stainless Steel Plate Shearing: How to Prevent Blade Material Contamination of the Product Surface?
    Aug 05, 2026
    In the slitting and processing of food-grade stainless steel plates, contamination of the product surface by blade materials is a serious challenge faced by many manufacturers. Once a blade rusts or wears, tiny metal particles can detach and embed themselves into the plate surface, causing the product to fail food safety standards and even posing risks of heavy metal migration. Mingbai Mechanical Tool Technology Co., Ltd., based on food contact material standards and years of slitting experience, provides a systematic analysis of how to eliminate contamination risks from the blade side.   1. Where Does Contamination Come From? — Analysis of Three Contamination Sources     1. Rust and metal dust contamination   During shearing, ordinary carbon steel or low-alloy steel blades produce fine iron filings that adhere to the surface of stainless steel plates. In humid environments, these iron filings oxidize and rust, forming yellow-brown rust spots that are difficult to remove, directly compromising the food-grade appearance and corrosion resistance of the plates.   2. Heavy metal element migration contamination   According to GB 4806.9-2016 "National Food Safety Standard — Metal Materials and Products for Food Contact," metal materials that come into direct contact with food must not cause harm to human health. Harmful elements such as lead, cadmium, and arsenic that may be present in ordinary blades can migrate to the product surface when in contact with food or humid environments.   3. Cross-contact contamination   After blades come into contact with carbon steel tools, workbenches, or other non-food-grade materials, their surfaces may become contaminated with iron ions or pollutants, which are then transferred to the stainless steel plates.   2. How to Eliminate Contamination from the Blade Side? — Five Core Measures   1. Select compliant food-grade blade materials   For food-grade stainless steel blade, blade materials must comply with GB 4806.9-2016. According to FDA regulations, the chromium content of food contact-grade stainless steel must be at least 16%.   Mingbai Technology recommends the following material options:   · Martensitic stainless steel (420, 440C): High hardness (HRC52-58), good edge retention, suitable for long-term shearing operations. According to GB 4806.9-2016, martensitic stainless steel materials can be used for the main body of stainless steel tableware and drilling and grinding tools of food production machinery. · Austenitic stainless steel (304, 316): Excellent corrosion resistance, suitable for humid or acidic environments. Among them, 316 contains molybdenum, providing stronger resistance to chloride ion corrosion. · Food-grade carbide: For high-hardness or impurity-containing stainless steel plates, ultra-fine grain carbide that meets food contact requirements can be used, combining wear resistance with safety.     2. Strictly control edge surface finish   Surface roughness directly affects the ability of contaminants to adhere and the difficulty of cleaning. The surface roughness Ra value of food contact surfaces should be less than 0.8μm. For high-hygiene applications, it is recommended to polish the edge to Ra ≤ 0.1-0.4μm, which significantly reduces adhesion and bacterial growth.   Mirror-polished food-grade stainless steel slitting blades from Mingbai Technology can achieve edge Ra values as low as 0.05μm, physically preventing contaminant adhesion.     3. Establish strict blade handling procedures   · Wear non-abrasive gloves: Food-grade blades must be handled with non-abrasive gloves (leather, Kevlar, or nitrile) to prevent sweat stains and oils from contaminating the blade surface. · Use dedicated handling tools: Use plastic, wooden, or stainless steel lifting tools when moving blades. Carbon steel tools must not come into contact with blades. · Dedicated blades for dedicated use: Food-grade blades must not be mixed with non-food-grade blades. Color-coded management is recommended to distinguish purposes.     4. Scientific blade storage management   · Dedicated blade racks: Use racks made of wood, plastic, or stainless steel, with each blade stored separately to avoid scratching from mutual contact. · Dust protection covers: Use blade covers during storage to prevent dust and foreign matter from adhering. · Environmental control: Storage area humidity should be controlled at 40%-60% to avoid rusting in humid environments.     5. Coating-assisted protection   For special working conditions, blades with food-grade coatings can be selected:   · DLC coating: Friction coefficient as low as 0.1, excellent anti-adhesion performance · TiAlN coating: Heat-resistant up to 800°C, suitable for high-speed slitting   Coatings not only reduce friction heat but also form a physical barrier between the blade substrate and the plate, further reducing the risk of metal migration.   3. Mingbai Technology's Food-Grade Slitting Blade Solutions   Mingbai Mechanical Tool Technology Co., Ltd. offers a dedicated blade series for food-grade stainless steel plate slitting:   · Food-grade stainless steel slitting dedicated blades: Made of 420/440C or 304/316 materials, compliant with GB 4806.9-2016 · Mirror-polished edge, Ra ≤ 0.05μm · Optional DLC/TiAlN food-grade coatings · Each batch of blades comes with material test reports and food contact safety declarations · On-site contamination risk assessment services   Conclusion   Contamination prevention in food-grade stainless steel plate shearing is a comprehensive battle from blade materials to operating procedures. Choosing the right blade material, controlling surface finish, standardizing handling and storage, and selecting appropriate coatings — every step is critical to the final product's food safety compliance. Mingbai Technology is ready to help you safeguard the first line of food safety with professional food-grade slitting blade solutions.     FAQ Module:   Q1: Can ordinary alloy blades be used for food-grade stainless steel plate shearing? A: Not recommended. Ordinary alloy blades may contain harmful elements such as lead and cadmium, and have insufficient corrosion resistance, making them prone to rusting and producing iron filings contamination. Blades must be made of food-grade stainless steel or carbide that complies with GB 4806.9-2016.   Q2: What surface finish is required for food-grade blades? A: The surface roughness Ra value of food contact surfaces should be less than 0.8μm. For high-hygiene food-grade stainless steel plate slitting, it is recommended to polish the edge to Ra ≤ 0.1-0.4μm. Mingbai Technology can provide mirror-grade edges with Ra ≤ 0.05μm.   Q3: Can a rusted blade continue to be used for food-grade plate shearing? A: No. Rusted blades produce rust dust that contaminates the plate surface, and rusted areas easily harbor bacteria. Once rust spots are found, the blade should be immediately taken out of service and professionally derusted or replaced.   Q4: What is the difference between food-grade stainless steel plates and ordinary stainless steel plates regarding blade requirements? A: Food-grade stainless steel plates have extremely high surface quality requirements. Any iron filing contamination, scratches, or rust spots can render the product non-compliant.Therefore, blades must be made of food-grade materials with excellent corrosion resistance, and edge finish must be much higher than ordinary slitting requirements.   Q5: Are coated blades safe for food-grade applications? A: As long as the coating material complies with food contact standards (e.g., GB 4806.10), they are safe. Coatings such as DLC and TiAlN are widely used in food processing. They not only reduce friction and adhesion but also form a physical barrier between the blade substrate and the plate, further reducing the risk of metal migration. All coated blades from Mingbai Technology comply with relevant food safety standards.   Website: www.mingbaiblade.com
  • Severe Burrs on Cut Edges During Stainless Steel Strip Slitting — How to Adjust the Edge Parameters of Slitter Blades?
    Aug 03, 2026
    In stainless steel strip slitting operations, severe burrs on the cut edge are one of the most common quality complaints. Faced with burrs, many operators only know how to "adjust the gap," but overlook the decisive impact of edge parameters themselves on burrs. Mingbai Mechanical Tool Technology Co., Ltd., based on years of stainless steel slitting experience, provides you with a systematic edge parameter adjustment solution.   1. Root Cause Analysis of Burrs in Stainless Steel Strip   Stainless steel has three characteristics — high toughness, high work-hardening tendency, and low thermal conductivity — making its slitting burr problem much more complex than that of ordinary carbon steel.   Main pathways of burr formation:   · Edge dulling → increased shear force → material tears rather than cuts → burrs increase · Improper edge angle → excessive cutting resistance → lateral material flow → edge roll-over burrs · Insufficient edge surface finish → high friction coefficient → material adhesion to edge → uneven burrs     2. Adjusting the Edge Angle   1. Reduce the edge angle (wedge angle)   The smaller the edge angle, the sharper the blade and the lower the cutting resistance. Recommended angles for sharp slitter blades for stainless steel strip slitting:   · Conventional stainless steel (304, 316): Wedge angle 22°-25° · High-hardness stainless steel (430, martensitic): Wedge angle 25°-28° · Ultra-thin stainless steel strip (<0.3mm): Wedge angle 18°-20°   Adjustment principle: Choose the smallest edge angle possible while ensuring edge strength. For every 2° reduction in angle, cutting resistance can be reduced by 10%-15%.   2. Increase the clearance angle   The clearance angle affects the friction area between the blade and material. For high-hardness wear-resistant slitter blades in stainless steel slitting, recommended clearance angles:   · Conventional conditions: 8°-10° · High-speed slitting (>100m/min): 10°-12° · High-adhesion stainless steel grades: 12°-15°     3. Edge micro-passivation   A sharp edge cuts easily but has a high risk of micro-chipping. High-speed steel circular slitting blade are recommended to be micro-passivated:   · Edge radius R=0.005-0.010mm (extremely sharp, suitable for thin strips) · Edge radius R=0.010-0.015mm (micro-passivated, suitable for conventional stainless steel) · Edge radius R=0.015-0.020mm (moderately passivated, suitable for thick strips or high-speed slitting)   3. Optimizing Edge Surface Finish   Edge surface finish is one of the key factors in controlling burrs.   Recommended standards:   · Edge surface roughness Ra ≤ 0.1μm (mirror grade) · Rake face (chip contact surface) Ra ≤ 0.2μm · Flank face (material contact surface) Ra ≤ 0.1μm   High-finish stainless steel slitting blades can effectively reduce material adhesion and lower burr height by 30%-50%.     4. Coordinated Adjustment of Side Gap and Edge Parameters   After adjusting edge parameters, the side gap should also be adjusted accordingly:   · Sharp edge + small gap (5%-7% of material thickness): suitable for precision slitting of thin strips · Micro-passivated edge + medium gap (7%-9% of material thickness): suitable for conventional stainless steel · Passivated edge + large gap (9%-12% of material thickness): suitable for thick strips or high-speed slitting   5. Auxiliary Improvement of Burrs Through Coating   Appropriate coatings can reduce friction and adhesion, indirectly improving burrs:   · TiAlN coating: Suitable for high-speed slitting, heat-resistant up to 800°C · DLC coating: Suitable for high-adhesion stainless steel, friction coefficient as low as 0.1 · CrN coating: Suitable for corrosive environments, excellent anti-adhesion performance   For anti-adhesion coated slitter blades, it is recommended to pair with a mirror-finished edge for better results.     6. On-Site Adjustment Procedure   1. First, inspect the existing edge angle and surface finish. 2. Calculate the recommended edge angle based on the stainless steel grade and thickness. 3. Return to the factory or perform on-site regrinding to achieve the target angle. 4. Polish the edge to Ra ≤ 0.1μm. 5. Reset the side gap. 6. Conduct a trial cut and observe burr changes. 7. Fine-tune until burrs meet the standard.   7. Mingbai Technology's Stainless Steel Slitting Blade Solutions   Mingbai Mechanical Tool Technology Co., Ltd. offers dedicated blades for stainless steel strip slitting:   · Stainless steel slitting dedicated slitter blades: Edge angle customizable according to working conditions. · Mirror-grade edge polishing, Ra ≤ 0.05μm. · Optional TiAlN/DLC/CrN coatings. · On-site edge parameter inspection and adjustment services.     Conclusion   Severe burrs on the cut edge during stainless steel strip slitting are often not an equipment problem, but a problem with the edge parameters themselves. By optimizing the edge angle, clearance angle, passivation value, surface finish, and coordinating with coating and side gap adjustments, burr issues can be effectively controlled. Mingbai Technology is ready to help you solve burr problems with professional stainless steel slitting blade solutions.   FAQ Module   Q1: How long does a resharpened edge last in stainless steel strip slitting? A: It depends on the stainless steel grade and slitting length. For conventional 304 stainless steel, one resharpening typically lasts for 5,000–10,000 meters of continuous slitting. It is recommended to inspect the edge every shift and resharpen as soon as burrs increase noticeably.   Q2: Is a smaller edge angle always better? A: No. A smaller angle makes cutting easier, but reduces edge strength. Too small an angle leads to chipping and shorter life. For stainless steel slitting, we recommend 22°–25°, with fine-tuning based on material thickness and equipment rigidity.   Q3: Do different stainless steel grades require different edge parameters? A: Yes. For austenitic grades like 304/316, use 22°–24° edge angle and 8°–10° clearance angle. For ferritic grades like 430, use 25°–27° edge angle and 10°–12° clearance angle. For high-hardness martensitic grades, use 28°–30° edge angle with moderate passivation.   Q4: Is there a big difference in burr control between coated and uncoated blades? A: Yes, a significant difference. With the same edge parameters, TiAlN or DLC coatings can reduce burr height by 30%–50%, reduce adhesion, and produce more uniform burrs. Coated blades are highly recommended for stainless steel slitting.   Q5: Which affects burrs more — side gap or edge parameters?   A: Both are equally important. Edge parameters determine cutting ability, while side gap determines the degree of tearing. The correct approach is to first optimize edge parameters, then fine-tune the side gap based on trial cut results. The two work together to achieve the best cut edge quality. Website: www.mingbaiblade.com
  • In Lithium Battery Electrode Slitting, Circular Blades Frequently Chip — How Can Material Optimization Solve This Problem?
    Jul 30, 2026
    In lithium battery electrode slitting operations, frequent chipping of circular blades is a persistent problem troubling many production lines. Chipping not only leads to excessive burrs and severe powder shedding on the electrode edge but can also puncture the separator, causing battery short-circuit risks. Many users first adjust equipment parameters, but Mingbai Mechanical Tool Technology Co., Ltd. tells you: the root cause of frequent chipping often lies in the mismatch between blade material and working conditions. This article provides a systematic solution from the material perspective.   1. Root Causes of Chipping in Electrode Slitting   Lithium battery electrodes consist of aluminum foil/copper foil current collectors and positive/negative electrode coatings. The coatings are hard and brittle. During slitting, circular blades must simultaneously cut through the coating and the metal foil, presenting a dual challenge of edge hardness and toughness.   Main causes of chipping include:   Impact from hard coating particles: Positive electrode materials such as lithium iron phosphate have high hardness, creating micro-impacts on the edge during cutting. Foil thickness fluctuations: Thickness deviations exceeding 3μm in the current collector cause uneven cutting forces. Insufficient blade toughness: Carbide is hard but brittle, with weak impact resistance. Edge micro-defects: Micro-cracks generated during grinding propagate under alternating stress.     2. Four Directions for Material Optimization   1. Select ultra-fine grain carbide substrate   Traditional carbide has coarser grains, and carbide particles are prone to detachment under impact, forming the starting point for chipping. Ultra-fine grain carbide circular blades for lithium battery electrode slitting use tungsten carbide powder with grain size ≤ 0.5μm, achieving hardness of HRA90-93 (equivalent to HRC68-75). The fine grain structure ensures more uniform carbide distribution, significantly improving resistance to micro-chipping. The ultra-fine grain substrate can increase transverse rupture strength by 20%-30%, fundamentally reducing chipping occurrence.     2. Match different carbide grades   Different electrode materials have different hardness requirements for blades:   Copper foil anode (negative electrode): Good ductility, requires higher blade toughness — recommended YG10X (HRA90.5). Aluminum foil cathode (positive electrode): High-hardness surface oxide layer — recommended YG12X (HRA91.5), which can extend life by 2.3 times compared to YG8 on aluminum foil. Coated electrodes: Coating materials are hard and brittle, requiring higher hardness blades with sharp edges.   3. Apply PVD coatings to enhance edge impact resistance   Coatings not only improve wear resistance but also reduce friction coefficient and reduce chipping caused by adhesion. High-hardness wear-resistant coated circular blades are highly effective in lithium battery slitting:   TiAlN coating: Reduces burr height by 35%-42% on copper foil electrodes. DLC coating: Reduces burrs by 50%-58% on aluminum foil electrodes, with a friction coefficient as low as 0.1 (uncoated is 0.4). TiCN coating: Reduces copper/aluminum adhesion by 40%.     4. Optimize edge geometry design   Edge angle directly affects chipping probability. High-precision electrode slitting circular blades are recommended with:   Edge angle 25°-35°, balancing sharpness and strength. Edge radius controlled within 3μm, maintaining sharpness while avoiding micro-chipping. Mirror finish grinding to Ra ≤ 0.1μm, with no chipping under 50-100x magnification.     3. Supporting Process Adjustment Recommendations   After material optimization, the following process adjustments are also recommended:   Blade gap: Controlled at 10%-20% of the total electrode thickness. Gap too large (>0.1mm) creates burrs; too small causes powder shedding. Slitting speed: Controlled at 60-120 m/min. Excessive speed increases friction heat. Regular inspection: Check the edge every 4 hours; if chipping >0.03mm, resharpening is needed.   4. Mingbai Technology's Electrode Slitting Blade Solutions   Mingbai Mechanical Tool Technology Co., Ltd. offers a dedicated blade series for lithium battery electrode slitting:   Ultra-fine grain carbide electrode slitting circular blades: Grain size ≤ 0.5μm, hardness HRA90-93. Optional TiAlN/DLC/TiCN coatings, matching the optimal solution for positive/negative electrode materials. Mirror finish edge grinding, no chipping under 50x magnification. Material selection recommendations and on-site working condition diagnosis.     5. Case Comparison   A lithium battery plant was slitting lithium iron phosphate positive electrode material. Ordinary carbide circular blades chipped every 2 hours, causing burrs to exceed tolerance. After switching to Mingbai Technology's ultra-fine grain carbide electrode slitting circular blades with TiAlN coating, the time between chipping events extended to 12 hours, blade life increased by 4 times, and electrode burrs were consistently controlled within 5μm.     Conclusion   Frequent chipping of circular blades in lithium battery electrode slitting often originates from the material. Systematic material upgrades — from ultra-fine grain carbide substrate, grade matching, PVD coatings, to edge geometry optimization — can significantly reduce chipping and extend blade life. Mingbai Technology is ready to help you overcome electrode slitting chipping challenges with professional material solutions. Website: www.mingbaiblade.com
  • After Long-Term Storage, Rust Spots Appear on the Cutting Edge of Circular Blades — Will This Affect Performance?
    Jul 28, 2026
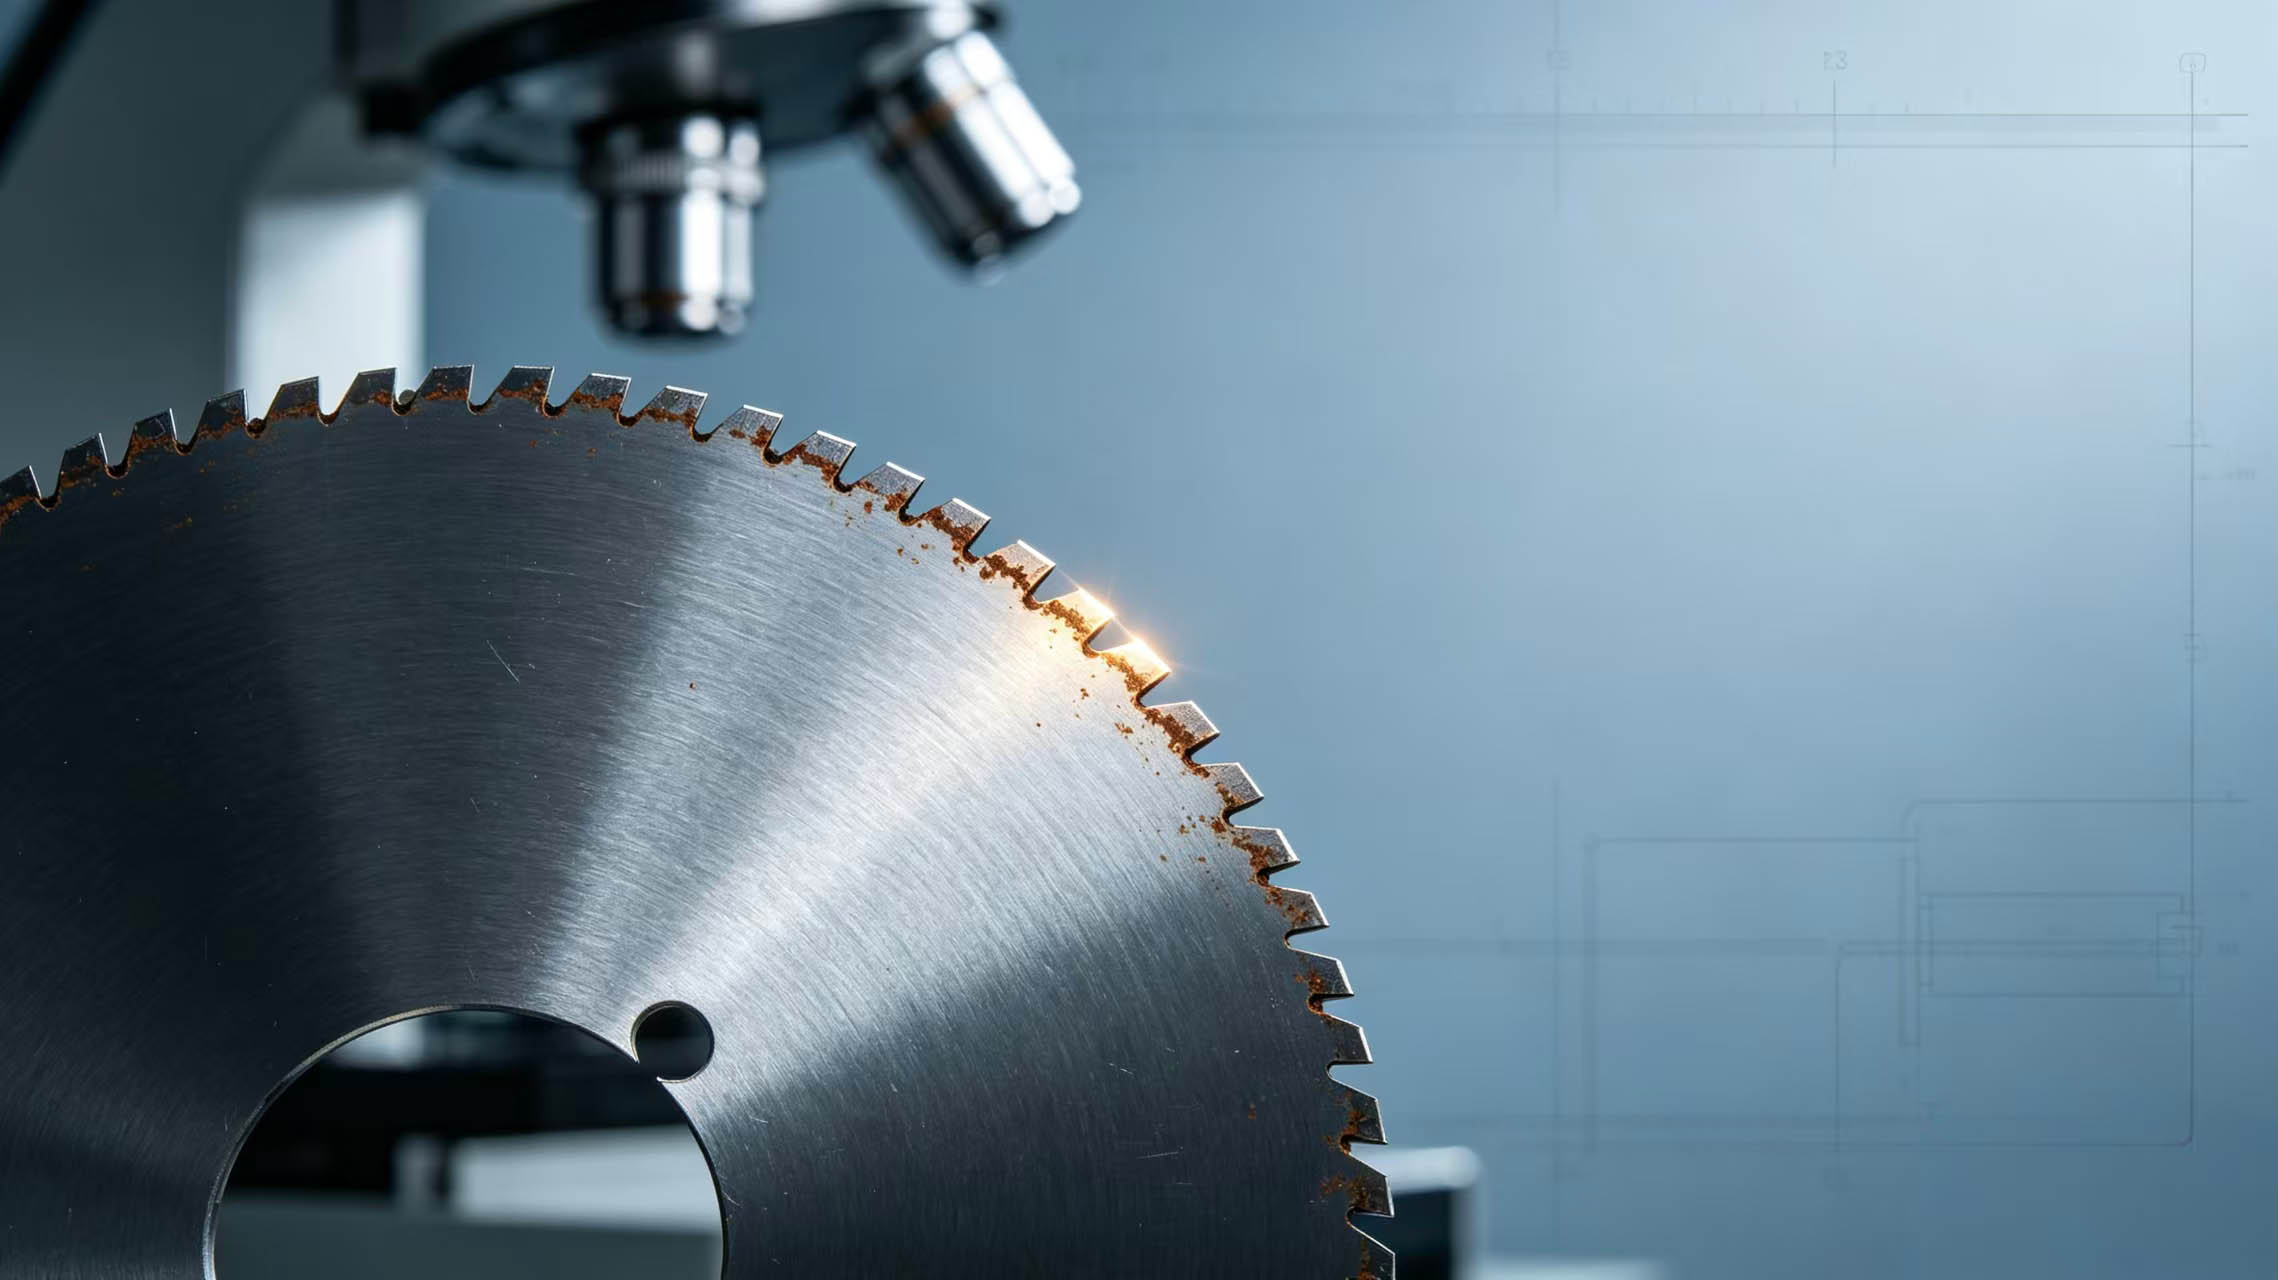
    In slitting production, many users retrieve circular blades from long-term warehouse storage and find yellowish-brown rust spots on the cutting edge. When faced with rust spots, the most common concern is: do these rust spots affect cutting performance? Can the blade still be used? Mingbai Mechanical Tool Technology Co., Ltd., based on materials science and field experience, provides scientific judgment criteria and handling recommendations.   1. The Nature and Hazards of Rust Spots   Rust spots are the product of electrochemical reactions between the blade's metal surface and oxygen and moisture in the air. For precision mechanical blades made of high-carbon steel, high-speed steel, and similar materials, once rusting begins, it penetrates from the surface inward. The harm of rust spots depends on three factors: location, depth, and morphology.   2. Three Types of Rust Spots on the Cutting Edge     Surface flash rust (mild) Characteristics: Yellowish-brown powdery rust, present only on the surface, depth < 0.01mm, removable with a cloth. Impact: After removal, no visible pits remain on the edge — does not affect performance.   Pitting rust (moderate) Characteristics: Dark brown or black spots, depth 0.01-0.03mm, leaving tiny pits the size of a pinprick after removal. Impact: May affect cutting quality, depending on specific working conditions.   Pitted/crater rust (severe) Characteristics: Dark brown or black depressions, depth > 0.03mm, leaving obvious pits or grooves after removal. Impact: Significantly affects performance, causing burrs or chipping during cutting — replacement is recommended.   3. Four-Step Method to Determine Whether Rust Spots Affect Performance   Step 1: Check the rust spot location   Rust spots on the cutting edge → directly affect cutting quality and require careful handling. Rust spots on the blade body (non-edge areas) → do not affect performance; clean and use. Inspection method for rust spots on stored circular blades starts with location.     Step 2: Assess rust spot depth   Gently sand the rusted area with fine sandpaper or an oilstone. If the surface is flat without pits after sanding → flash rust, can continue to be used. If obvious pits remain → rust has penetrated the substrate; assess whether edge integrity is compromised.     Step 3: Check edge integrity   Use a magnifying glass to inspect the edge. If the edge remains straight and intact → rust has not damaged the edge geometry. If the edge appears jagged or has notches → rust has damaged the edge, and circular blades for precision slitting will directly affect cutting accuracy.     Step 4: Verify through trial cutting   After cleaning the rust, perform a trial cut. Smooth cut edge without burrs → performance restored. Obvious burrs or uneven edges → rust has affected performance; recommend replacement or return to factory for regrinding.     4. Rust Tolerance of Different Blade Materials   High-speed steel circular blades: Most sensitive to rust. Pitting deeper than 0.02mm is recommended for replacement.   Carbide blades: The substrate does not rust, but the cobalt binder phase may corrode; edge strength must be checked.   Stainless steel blades: Good corrosion resistance. Rust spots usually stay on the surface with shallow depth. Ultra-thin circular blades for food packaging film slitting are more sensitive to defects and require special attention.   Coated blades: Rusting tends to occur where the coating is damaged; confirm whether rust has penetrated the coating.   5. Rust Removal Methods   Flash rust removal Gently sand with a fine oilstone (1000 grit or higher) with oil, or lightly brush with a brass wire brush, then wipe with rust preventive oil for protection.   Moderate rust removal Sand with fine sandpaper (800-1200 grit) until the surface is bright, taking care not to alter the edge geometry. Then inspect edge integrity with a magnifying glass.   Deep rust treatment Directly scrap, or send back to Mingbai Technology for evaluation to see if it can be restored through regrinding. If the edge is intact after regrinding, it can continue to be used.   6. How to Prevent Rust Spots in Storage?   · Control storage environment humidity between 40%-60%. · Long-term stored custom slitter blades should be coated with rust preventive oil and vacuum-packed. · Regularly inspect inventory, spot-check every 3 months. · Store blades of different materials separately to avoid galvanic corrosion.     7. Mingbai Technology's Rust Inspection Services   Mingbai Mechanical Tool Technology Co., Ltd. offers rust evaluation for stored circular blades services:   · Free visual inspection to determine rust type and depth. · Microscope inspection of edge integrity. · Provide repair or replacement recommendations. · Professional rust removal and regrinding services for repairable blades.   Conclusion   Rust spots on the cutting edge of circular blades after long-term storage do not necessarily mean the blade is scrap. Surface flash rust can be cleaned and does not affect performance. Pitting rust requires assessment of location and depth. Pitted/crater rust or edge damage should be scrapped or sent back for repair. The key steps are: "check location, measure depth, inspect edge, verify through trial cutting." Mingbai Technology is ready to provide professional rust inspection and repair services for you. Website: www.mingbaiblade.com
  • After Alloy Blade Chipping, How Many Times Can It Be Reground?
    Jul 22, 2026
    In slitting production, alloy blades often need regrinding due to chipping. Many users ask: after chipping, how many times can an alloy blade be reground? Will too many regrinds ruin it? Mingbai Mechanical Tool Technology Co., Ltd., based on materials science and resharpening experience, provides clear answers and judgment standards.   1. The Nature of Chipping   Chipping refers to small pieces of material breaking off from the cutting edge due to impact or fatigue, with depths ranging from 0.05mm to several millimeters. The purpose of regrinding is to remove the chipped layer and re-form a complete edge geometry. However, each regrinding consumes blade thickness. When the remaining thickness is insufficient to support normal cutting, the blade reaches the end of its life.     2. Four Factors Affecting the Number of Regrinds   1. Original blade thickness   Thicker blades can withstand more regrinds. For example, a carbide blade with 5mm thickness has several times more regrinding potential than a 2mm blade.   2. Chipping depth   Deeper chips require more material removal per regrind, resulting in fewer total regrinds. A 0.1mm chip can be removed with minimal grinding; a 1mm chip may require a significant amount of material removal in a single pass.   3. Grinding method   CNC grinding machines can precisely control each regrind removal amount (0.05-0.1mm), maximizing blade life. Manual grinding with a hand grinder is difficult to control and often results in excessive material removal.   4. Blade material   Different alloy blade materials have varying tolerance to grinding. Carbide blades for stainless steel strip slitting require more careful grinding due to their high hardness to avoid thermal cracks.   3. Reference Regrinding Counts for Different Blade Thicknesses     Thick alloy blades (thickness ≥ 8mm):   · Light chipping (<0.2mm): 8-12 regrinds · Moderate chipping (0.2-0.5mm): 5-8 regrinds · Severe chipping (>0.5mm): 3-5 regrinds   Medium alloy blades (thickness 4-8mm):   · Light chipping: 5-8 regrinds · Moderate chipping: 3-5 regrinds · Severe chipping: 2-3 regrinds   Thin alloy blades (thickness < 4mm):   · Light chipping: 3-5 regrinds · Moderate chipping: 2-3 regrinds · Severe chipping: recommended to scrap directly   4. When Should Regrinding Be Stopped?   1. Insufficient remaining thickness   When the remaining blade thickness is less than 60%-70% of the original thickness, the edge support strength decreases, making it prone to further chipping. Alloy blades for precision slitting are particularly sensitive to thickness changes.   2. Hardness drop after multiple regrinds   Each regrind generates heat. If cooling is insufficient, micro-cracks or hardness reduction may occur on the edge surface. Alloy blades for high-speed slitting should undergo hardness spot checks after multiple regrinds.   3. Blade deformation   After multiple regrinds, the blade may develop cumulative deformation (end face warping, flatness out of tolerance). If deformation exceeds 0.02mm, regrinding should be stopped.   4. Abnormal chip location   If chipping repeatedly occurs at the same location, it may indicate an internal defect in the blade. Continued regrinding will not solve the fundamental problem.   5. How to Maximize the Number of Regrinds?   1. Remove only the minimum necessary each time: Remove just enough to eliminate the chip; do not grind "just because." 2. Use a CNC grinder: Precisely control the removal amount and angle. 3. Ensure adequate cooling: Avoid grinding burns. 4. Record each regrind removal amount: When cumulative removal exceeds 15%-20% of the original thickness, consider replacement.   6. Mingbai Technology's Regrinding Services   Mingbai Mechanical Tool Technology Co., Ltd. offers professional alloy blade regrinding services:     · CNC grinding machines with angle control of ±0.3°. · Precise control of single regrind removal (0.03-0.10mm). · Hardness testing before and after regrinding to ensure no annealing. · Microscope inspection of the edge after regrinding to ensure no micro-cracks. · Provision of regrinding records to track each regrind removal amount and remaining thickness.     7. Case Study   A precision strip slitting plant used alloy blades for precision strip slitting with an initial thickness of 6mm. The first chip depth was 0.15mm. Mingbai Technology used a CNC grinder with 0.06mm removal per regrind. After a cumulative 9 regrinds, the remaining thickness was 4.8mm, still meeting cutting quality requirements, achieving a total life 2.5 times that of a new blade.     Conclusion   There is no fixed answer to how many times an alloy blade can be reground after chipping. It depends on the original thickness, chipping depth, grinding method, and blade material. However, by adopting a strategy of "remove only the minimum necessary + CNC precision control + adequate cooling," most alloy blades can be reground 5-10 times. Mingbai Technology is ready to help you maximize blade life with professional regrinding services. Website: www.mingbaiblade.com
  • Is There a Universal Calculation Formula for the Side Gap Between Upper and Lower Slitter Blades?
    Jul 20, 2026
    In metal slitting operations, the side gap (also called lateral clearance) between slitter blades is one of the most critical process parameters. If the side gap is too large, the cut edge becomes jagged with burrs. If the side gap is too small, the blades rub against each other, generate heat, and may even chip. So, is there a universal calculation formula to quickly determine a reasonable side gap value? Mingbai Mechanical Tool Technology Co., Ltd., based on domestic and international standards and years of practice, provides you with a scientific calculation method.   1. The Universal Calculation Formula for Side Gap   The core of side gap calculation is the "material thickness percentage method," with the formula as follows:   Side Gap C = K × t     Where:   · C = Side gap (mm) · K = Gap coefficient (dimensionless) · t = Thickness of the material being sheared (mm)   Principles for selecting K value:   · Hard and brittle materials (silicon steel, high-carbon steel): K = 8%-12% · Soft and tough materials (low-carbon steel, copper, aluminum): K = 5%-7% · Medium hardness materials (ordinary carbon steel, stainless steel): K = 6%-10% · Ultra-thin materials (<0.3mm): K = 3%-5%   2. Recommended K Values for Different Materials     Ordinary carbon steel (Q235, SPCC, DC01): K = 6%-8%. Use the lower limit for thin materials (0.5mm at 6%) and the upper limit for thick materials (3mm at 8%). Circular blades for ordinary carbon steel slitting should be set according to this coefficient.   Stainless steel (304, 316, 430): K = 8%-10%. Stainless steel has severe work hardening, so a larger gap reduces friction between the edge and the material. Wear-resistant circular blades for stainless steel strip slitting are recommended with K = 9%.   Silicon steel: K = 10%-12%. The material is hard and brittle, requiring a larger gap to reduce impact. Alloy blades for silicon steel slitting are recommended with K = 11%.   Non-ferrous metals such as copper and aluminum: K = 4%-6%. Soft metals are sensitive to gap; too large a gap causes edge stringing. Circular blades for copper strip cutting are recommended with K = 5%.   High-strength steel: K = 8%-10%. Balancing hardness and toughness, the gap should not be too small. Custom blades for automotive panel slitting are recommended with K = 9%.   3. Other Factors Affecting K Value   1. Equipment rigidity   For equipment with good rigidity, the K value can be taken at the lower limit. For equipment with poor rigidity, use the upper limit to absorb impact.   2. Shearing speed   At high speeds (>100m/min), the K value should be reduced by 10%-15% compared to the conventional value to reduce vibration and temperature rise.   3. Blade material   Carbide blades, due to their high hardness and low deformation, can use a K value 5%-10% smaller than high-speed steel blades. High-hardness alloy blades can have a slightly smaller gap under the same working conditions.   4. Adjustment Method in Practical Application   Step 1: Calculate the initial gap using the formula   For example, for shearing 2.0mm thick 304 stainless steel, t = 2.0mm, K = 9%, then C = 2.0 × 9% = 0.18mm.   Step 2: Verify through trial cutting   Slit a section of material at normal speed and inspect the cut edge with a magnifying glass:     · Small, uniform burrs → gap is appropriate · Large burrs with tearing marks → gap is too large; reduce by 0.01-0.02mm · Whitened edge with powder → gap is too small; increase by 0.01-0.02mm   Step 3: Record the optimal value   Record the verified optimal gap value on the process card for direct use next time.   5. Five Precautions for Gap Adjustment   1. After each blade or material change, the gap must be re-measured and adjusted. 2. Use a feeler gauge for measurement; do not estimate by "feel."     3. After upper and lower blades are resharpened, the outer diameter becomes smaller, and the gap must be reset. 4. In multi-blade slitting, the gap for each blade should be consistent. 5. The gap adjustment precision for precision mechanical blades should be controlled within ±0.005mm.   6. Mingbai Technology's Gap Setting Services   Mingbai Mechanical Tool Technology Co., Ltd. provides side gap calculation and optimization services:   · Free calculation of recommended gap values based on your material, equipment, and speed. · On-site guidance for gap adjustment and trial cut verification. · Supply of high-precision feeler gauges and gap measurement tools. · For custom slitter blades, the gap value can be preset according to your working conditions.     7. Case Study   A stainless steel strip slitting plant used the same set of wear-resistant circular blades for stainless steel strip slitting to shear 1.0mm and 2.0mm stainless steel. The operator consistently used a 0.08mm gap for both thicknesses. As a result, the 1.0mm material cut well, but the 2.0mm material had severe burrs. Mingbai engineers calculated using the formula: 1.0mm × 9% = 0.09mm, 2.0mm × 9% = 0.18mm. After setting the gaps separately, the cut edge quality met standards for both thicknesses.   Conclusion   Although there is no "universal formula" for slitter blade side gap, the "C = K × t" calculation method covers the vast majority of working conditions. The key is selecting the K value — based on material, equipment, and speed, then fine-tuning through trial cuts. Mingbai Technology is ready to help you find the most suitable gap value with professional calculations and on-site services. Website: www.mingbaiblade.com
  • Mechanical Blade Hardness Meets the Standard, but Why Is Its Service Life Still Shorter Than Others?
    Jul 14, 2026
    In slitting production, many users encounter a puzzling phenomenon: the hardness test report for mechanical blades shows that the HRC value fully meets the requirements, but the actual service life is far lower than that of peers or expectations. Hardness meets the standard, but life does not — where does the problem lie? Mingbai Mechanical Tool Technology Co., Ltd., based on extensive field cases, reveals six "invisible killers" beyond hardness.   1. Hardness Is Only a "Passing Line," Not a "Guarantee"   Hardness is a basic indicator of blade wear resistance, but it only represents the material's ability to resist indentation deformation. The actual service life of a blade also depends on multiple factors such as toughness, fatigue resistance, microstructure, and edge condition. Just like a medical report showing "all indicators normal" doesn't mean a person can run a marathon — hardness meeting the standard is just "passing," and longevity depends on other "subjects."   2. Six Hidden Factors Affecting Service Life   1. Substandard metallographic structure   With the same hardness, different metallographic structures can result in more than double the difference in service life. For example, in Cr12MoV blades both at HRC60, those with well-distributed fine carbides have far superior wear resistance to those with coarse, aggregated carbides. High-speed steel blades for precision slitting with carbide segregation have edges that are like "a mosaic of hard and soft" at the microscopic level — the soft areas wear first, forming microscopic serrations that accelerate overall failure.     2. Edge micro-defects   Even when hardness meets the standard, micro-chipping, grinding cracks, or stress concentration points on the edge can rapidly propagate during shearing, leading to premature edge failure. High-hardness alloy blades have relatively poor toughness despite their high hardness, making them more sensitive to edge micro-defects.     3. Mismatched or poor-quality coating   With the same substrate hardness, the presence, type, and quality of coating have a significant impact on service life. Wear-resistant coated circular blades can have a life 2-5 times longer than uncoated blades. However, if the coating has poor adhesion, uneven thickness, or incorrect selection, it may not only fail to extend life but actually accelerate failure.     4. Poor resharpening quality   Blades need resharpening to restore sharpness after use. However, if the feed rate is too fast or cooling is insufficient during resharpening, the edge can suffer from "grinding burn" — the hardness may appear unchanged, but micro-cracks and residual stress have already formed on the surface. The resharpening quality of custom blades directly determines the degree of life recovery after resharpening.     5. Improper installation and gap setting   Eccentric blade installation, excessive or insufficient gap, can cause abnormal localized stress on the edge. High-speed slitter blades with too small a gap cause edge friction and micro-thermal cracks; with too large a gap, the edge bears additional impact loads. These abnormal stresses accelerate edge failure, regardless of hardness.     6. Matching of working conditions and material   Hardness and working conditions need to match. Wear-resistant circular blades for stainless steel strip slitting perform excellently in stainless steel slitting, but if used on glass fiber-containing composites, even the highest hardness will wear rapidly. Hardness meeting the standard does not mean a "universal blade" — the matching between material and working conditions is what really matters.   3. How to Diagnose the Real Cause of Short Life?   · Conduct metallographic analysis: check carbide distribution, grain size, and retained austenite content. · Inspect edge condition: use a magnifying glass or microscope to check for micro-chipping or grinding cracks. · Evaluate coating quality: check coating thickness, adhesion, and uniformity. · Review resharpening records: confirm whether resharpening parameters were reasonable and whether grinding burns occurred. · Check installation precision: verify concentricity, gap, and runout meet standards.     4. Mingbai Technology's "Full-Element" Life Guarantee   Mingbai Mechanical Tool Technology Co., Ltd. does not just promise hardness compliance — we provide a "full-element" life guarantee:   · Each batch of blades comes with a metallographic inspection report (carbide grade, grain size). · 100% edge inspection under microscope to ensure no micro-defects. · Coating thickness and adhesion test reports. · Resharpening process parameter recommendations to avoid resharpening damage. · On-site installation guidance to ensure gap and concentricity compliance.   5. Case Comparison   A precision strip slitting plant used carbide blades from two suppliers, both with a hardness of HRC62. Supplier A's blades lasted 3 days, while Supplier B's lasted 7 days. Mingbai Technology's inspection found: Supplier A's blades had a carbide grade of 5 (coarse aggregation), while Supplier B's had a grade of 2 (fine and uniform). Same hardness, different microstructures — more than double the difference in life.   Conclusion   When mechanical blade hardness meets the standard but life is short, the problem is often not the hardness itself, but the "invisible killers" beyond hardness — metallographic structure, edge defects, coating quality, resharpening damage, installation precision, and working condition matching. Mingbai Technology's "full-element" quality control ensures that every blade not only meets hardness standards but also delivers long-lasting durability. Website: www.mingbaiblade.com
  • When Customizing Blades, Why Is There Always a Deviation Between the "Edge Angle" Marked on the Drawing and the Actual Machined Result?
    Jul 13, 2026
    When customizing custom blades, circular blades, or slitter blades, many customers encounter a puzzling problem: the edge angle is clearly marked on the drawing, but the actual machined blade always deviates from the drawing when measured. Is it due to insufficient machining precision on the manufacturer's side? Or is there a problem with the drawing itself? Mingbai Mechanical Tool Technology Co., Ltd., based on years of production experience, explains six common causes of angle deviation.   1. Different Measurement References — The Angle on the Drawing and the Actual Measured Angle Are Not the Same "Angle"   The edge angle is a three-dimensional geometric concept. The angle marked on the drawing is usually a theoretical value measured on a specific cross-section, such as a plane perpendicular to the edge direction. However, during actual measurement, if the measurement direction, cross-section position, or measuring instrument differs, the obtained values will vary.   For example, for circular blades for precision slitting, the edge angle is measured on the normal cross-section at the highest point of the edge. If the measurement is offset by 0.5mm, the angle can differ by 1°to 2°.   2. The Effect of Edge Radius (Passivation Value)   The edge angle marked on the drawing usually assumes an ideal sharp edge (R=0). In reality, all blades have a certain edge radius after grinding. Alloy blades for high-speed slitting are often micro-passivated (R=0.01-0.02mm), and this passivation makes the actual measured "apparent angle" slightly larger than the theoretical angle.     3. Thermal Deformation During Grinding   Grinding generates heat, causing localized temperature rise and metal expansion. After cooling, the blade contracts, but the contraction amount varies across different areas, potentially causing minor changes in the edge angle. Ultra-thin mechanical blades are particularly sensitive to thermal deformation; even with adequate cooling during grinding, deviations of 0.5° to 1° can still occur.   4. Grinding Wheel Wear and Dressing Frequency   In batch production, the grinding wheel gradually wears. If not dressed in time, the wheel's shape changes, causing the ground edge angle to drift accordingly. Wear-resistant circular blades for stainless steel strip slitting require extremely high angle consistency, and accumulated angle deviation due to wheel wear can reach ±1.5°.     5. Measuring Instrument Precision and Calibration   Different measuring instruments have different precision and calibration status. Measuring the same blade's edge angle with a projector, tool microscope, or profilometer can yield differences of 0.5° to 1°. If instruments are not regularly calibrated, the deviation is even larger.     6. Incomplete Drawing Specifications   Many drawings only specify "edge angle 30°" without indicating whether it is the wedge angle, rake angle, or clearance angle, nor do they specify the measurement cross-section, tolerance range, or edge radius requirements. For high-hardness custom blades, if the edge angle lacks a tolerance specification, the manufacturer will follow default standards such as ±2°, which may deviate significantly from the customer's expectations.   7. How to Avoid Angle Deviation? — Five Suggestions   1. Complete drawing specifications Clearly specify the values of wedge angle, rake angle, and clearance angle; indicate the measurement cross-section position; specify the angle tolerance (recommended ±0.5°); and state the edge radius requirements.   2. Agree on measurement method Confirm with the manufacturer what instrument will be used and at what cross-section position the measurement will be taken, ensuring both parties have a consistent understanding of "angle."   3. Request first-article inspection Before mass production, ask the manufacturer to provide a first-article inspection report to confirm the angle meets requirements before proceeding with batch production.   4. Choose a manufacturer with CNC grinding capability CNC grinders can precisely control the grinding wheel path, keeping angle deviation within ±0.3°.   5. Consider grinding allowance For custom slitter blades, you may specify "grinding allowance 0.1-0.2mm" on the drawing to allow for final precision grinding and angle adjustment.   8. Mingbai Technology's Angle Control Capability   Mingbai Mechanical Tool Technology Co., Ltd. uses five-axis CNC grinders, achieving edge angle control precision of ±0.3°. Every precision mechanical blade is inspected with a profilometer before shipment, and an angle inspection report is provided. We guarantee that the deviation between the drawing-specified angle and the actual machined angle is ≤±0.5° (and can be controlled within ±0.3° for special cases).   Conclusion   The deviation between the edge angle marked on the drawing and the actual machined result can stem from multiple factors: measurement reference, edge radius, thermal deformation, wheel wear, instrument precision, or incomplete drawing specifications. As long as both parties agree on specification, measurement, and inspection, the deviation can be controlled within an acceptable range. Mingbai Technology is committed to precision manufacturing, ensuring your drawing and the actual product match "angle for angle." Website: www.mingbaiblade.com
  • Circular Blade Bore Wear Exceeds 0.05mm — Should It Be Repaired or Directly Scrapped?
    Jul 07, 2026
    In slitting production, circular blades transmit torque through the bore fit with the blade shaft. After long-term use, the bore wall gradually enlarges due to fretting wear and repeated mounting and dismounting. When bore wear exceeds 0.05mm, many users face a dilemma: repair with concerns about precision, or scrap with regret over waste. Mingbai Mechanical Tool Technology Co., Ltd. provides professional judgment criteria and repair solutions.   1. Three Degrees of Bore Wear     Light wear (<0.03mm): The bore size remains near the upper tolerance limit, and the blade shows no obvious play after installation. In this case, simply replacing the spacer or applying anti-loosening adhesive is sufficient; no repair is needed.   Moderate wear (0.03-0.05mm): The clearance between the bore and blade shaft has increased noticeably, and radial play can be felt after installation. During shearing, periodic burrs appear on the material edge, and width fluctuations increase. At this point, the repair value needs to be assessed.   Severe wear (>0.05mm): The bore has become significantly out-of-round or flared. After installation, the blade is severely eccentric, causing violent vibration during shearing and obvious wavy edges on the product. Repair is difficult at this stage and requires careful decision-making.   2. Repair or Scrap? Five Judgment Dimensions   1. Residual blade value   If heavy-duty circular blades for high-speed slitting still have more than 3 resharpening allowances left, and the blade has high original value (e.g., carbide or powder metallurgy high-speed steel wear-resistant carbide circular blades), repair is worthwhile. If the edge is near the end of its life, scrapping is more economical.   2. Equipment precision requirements   Ordinary slitting lines (with precision tolerance of ±0.1mm) have higher tolerance for repaired bore precision. High-precision circular blades for precision strip slitting have stringent concentricity requirements and must be strictly inspected after repair.   3. Wear pattern   Uniform enlargement (wear amount similar across all areas) → repairable. One-sided wear or flaring → repair is difficult and requires evaluation. Cracks or chipping at the bore edge → scrap immediately.   4. Blade type   For coated alloy blades, care must be taken not to damage the coating during bore repair; professional factory repair is recommended. For custom blades, repair is often the better choice due to lack of off-the-shelf replacements.   5. Repair cost   Repair cost is typically 15%-30% of a new blade. If the repaired blade can achieve over 70% of new blade life, repair is cost-effective.   3. Three Repair Methods   1. Bore brush plating (chrome/nickel plating)   Electrodeposit a layer of metal on the worn bore surface to restore dimensions. Advantages: no change to the blade substrate, low temperature, no deformation. Disadvantages: limited coating hardness, not suitable for heavy-load conditions. Suitable for mechanical blades for medium-load slitting.     2. Bore sleeve insertion   Enlarge the original bore by 0.5-1mm, press in a heat-treated inner sleeve, and finish-machine the new bore to original dimensions. Advantages: restores original fit precision, long life. Disadvantages: higher cost, requires professional equipment. Suitable for heavy-duty alloy blades.     3. Bore overlay welding + re-machining   Use special welding rods to build up the bore wall, then re-bore to original dimensions. Advantages: metallurgical bonding of the repair layer with the substrate. Disadvantages: significant heat-affected zone, may cause deformation. Suitable for circular blades for thick plate slitting.   4. Three Situations Requiring Scrapping   · Cracks at the bore edge (even if very small) · The blade has been resharpened more than 5 times, and the remaining effective thickness is insufficient · Severe bore out-of-roundness (ellipticity >0.03mm) and concentricity error >0.03mm   5. Verification Standards After Repair     A repaired precision mechanical blade must pass the following inspections before installation:   · Bore size restored to original tolerance (H7 or H6) · Bore roundness ≤ 0.003mm · Bore-to-end-face perpendicularity ≤ 0.005mm · Radial runout after shaft mounting ≤ 0.008mm   6. Mingbai Technology's Repair Services   Mingbai Mechanical Tool Technology Co., Ltd. offers circular blade bore wear repair services:   · Bore brush plating (controllable coating thickness, restoring to original dimensions) · Bore sleeve insertion (professional press-fit, interference fit) · Post-repair CMM inspection with precision report · Quality guarantee: 100% pass rate for assembly after repair, otherwise free rework     Conclusion   When circular blade bore wear exceeds 0.05mm, whether to repair depends on residual blade value, equipment precision requirements, wear pattern, and repair cost. Light wear requires no treatment, moderate wear can be repaired, and severe wear or cracks should be decisively scrapped. Mingbai Technology is ready to help you extend blade life and reduce tooling costs with professional repair techniques and inspection capabilities. Website: www.mingbaiblade.com
  • Why Do Stainless Steel Blades Always Produce Built-Up Edge at the Cutting Edge During Shearing?
    Jul 06, 2026
    In stainless steel strip slitting operations, a sticky accumulation resembling a "tumor" often appears on the cutting edge of stainless steel blades — this is known as built-up edge. It is formed by tiny metal particles from the sheared material that cold-weld onto the edge surface under high temperature and pressure. Built-up edge not only roughens the cut edge and increases burrs but also accelerates edge wear and, in severe cases, can cause chipping. Mingbai Mechanical Tool Technology Co., Ltd., based on years of stainless steel slitting experience, analyzes the causes of built-up edge and provides solutions.   1. Formation Mechanism of Built-Up Edge     Stainless steel has high toughness, high work-hardening tendency, and low thermal conductivity. During shearing, intense friction occurs between the edge and the material, causing temperatures to rise sharply (locally reaching 500-800°C). Under high temperature and pressure, elements such as chromium and nickel in the stainless steel undergo a "cold welding" effect with the edge surface, and material particles gradually adhere and accumulate, forming built-up edge.     The growth of built-up edge is dynamic: it continuously grows and periodically detaches. When it detaches, it may take away edge material, causing edge defects.   2. Why Is Stainless Steel Particularly Prone to Built-Up Edge?   · High adhesion: The chromium content in stainless steel makes its surface prone to adhesion with blade materials. · Low thermal conductivity: Heat is concentrated in the edge area, accelerating adhesion. · Work hardening: The material rapidly hardens during shearing, increasing friction and further raising temperatures.   3. Five Causes of Built-Up Edge Formation   1. Insufficient edge surface finish   The rougher the edge surface, the more microscopic peaks and valleys exist, making it easier for stainless steel particles to "anchor" in the pits and gradually accumulate into built-up edge. Stainless steel blades for precision slitting require edge surface roughness Ra ≤ 0.1μm; otherwise, built-up edge is highly likely to form.     2. Edge angle too small   An excessively small edge angle (<18°) results in insufficient edge strength. During stainless steel shearing, the edge undergoes micro-deformation, increasing contact area with the material and intensifying friction, making built-up edge formation easier. High-speed steel custom blades require an edge angle of 22°-25° for stainless steel slitting.   3. Insufficient lubrication and cooling   Stainless steel slitting requires adequate cooling and lubrication. Insufficient cooling leads to excessive temperatures; insufficient lubrication increases the friction coefficient — both promote built-up edge growth.   4. Improper shearing speed   At low speeds, the material stays at the edge too long, causing heat accumulation; at high speeds, friction heat increases sharply. Each stainless steel grade has its optimal shearing speed window.   5. Mismatched blade coating   TiN coatings tend to adhere to stainless steel during slitting. Wear-resistant coated alloy blades are better suited with TiAlN or AlCrN coatings, which offer superior high-temperature stability and anti-adhesion performance.     4. Three Typical Stages of Built-Up Edge   · Initial stage: Tiny white spots appear on the edge, and fine burrs begin to form on the cut edge. · Intermediate stage: Built-up edge grows larger, burrs become noticeable, and the cut surface becomes rough. · Advanced stage: Built-up edge detaches, taking edge material with it, resulting in chipping.     5. Six Effective Measures to Eliminate Built-Up Edge   1. Improve edge surface finish Polish the edge surface to Ra ≤ 0.05μm to reduce microscopic anchoring points. Mirror-polished stainless steel blades are highly effective in high-end slitting applications.   2. Optimize edge angle Recommended edge angle for stainless steel slitting: 22°-25°, clearance angle 8°-10°, with micro-passivation (R=0.01-0.02mm).   3. Select the appropriate coating TiAlN or AlCrN coatings offer excellent anti-adhesion properties, reducing built-up edge formation. High-hardness wear-resistant coated circular blades perform excellently in stainless steel slitting.   4. Optimize cooling and lubrication Use stainless steel-specific cutting fluid, ensure nozzles are aimed at the cutting entry zone, and maintain sufficient flow (oil mist lubrication 10-20ml/h recommended).   5. Adjust shearing speed Recommended speeds: 80-120m/min for 300 series stainless steel, 60-100m/min for 400 series; fine-tune according to specific grades.   6. Regularly inspect the edge Inspect the edge during each shift change. If early signs of built-up edge are found, clean them promptly to prevent severe adhesion.   6. Mingbai Technology's Anti-Adhesion Solutions   Mingbai Mechanical Tool Technology Co., Ltd. offers a dedicated blade series for stainless steel slitting:   · Anti-adhesion stainless steel slitting blades: featuring mirror polishing + PVD AlCrN coating · Edge surface roughness Ra ≤ 0.05μm · Optional micro-lubrication system for optimal lubrication · Edge condition inspection services to monitor built-up edge development     7. Case Study   A precision stainless steel strip slitting plant used ordinary alloy blades to slit 304 stainless steel. Visible built-up edge appeared on the edge every 2 hours, and cut edge burrs exceeded tolerance. After switching to Mingbai Technology's anti-adhesion stainless steel slitting blades, the time before built-up edge appeared extended to 12 hours, blade life increased by 3 times, and cut edge quality remained stable.   Conclusion   The root cause of built-up edge formation when shearing with stainless steel blades lies in the high adhesion characteristics of stainless steel and the microstructure of the edge surface. Effective control requires a multi-pronged approach: improving surface finish, optimizing angles, selecting suitable coatings, and improving lubrication. Mingbai Technology is ready to help you eliminate built-up edge problems with professional stainless steel slitting blade solutions. Website: www.mingbaiblade.com
1 2 3 4 5 6 7 8
Leave A Message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
submit

leave a message

leave a message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
submit

home

products

WhatsApp

Contact Us